- This topic is empty.
-
AuthorPosts
-
2026-10-29 at 4:17 pm #12946
Published: October 2026 | By Kunda Metal Engineering Team
A solenoid valve housing does four jobs at once: it completes the magnetic circuit as the return path, it sets and holds the working air gap, it contains the pressurized medium, and it locates the valve in the manifold. That list is the short answer to what does a solenoid valve housing actually do — and each item maps to tolerances most drawings leave out. A housing that is dimensionally perfect but magnetically wrong passes CMM and still fails a pull-force test.
Most housings are bought by weight and specified by grade, thickness and a handful of dimensions — until the end-of-line test shows holding force 15% low at 120 °C and the coil, which is fine, gets blamed. Below is how our engineers at Kunda Metal split the housing into its four functions when a custom project starts — and what each one demands from the drawing.
1. Which four functions does a solenoid valve housing perform?
The housing performs four functions: magnetic return path, air-gap definition, pressure containment, and location. Each one fails in a different way, and each needs its own callouts.
Function 1 — It closes the magnetic circuit
The coil creates magnetomotive force, but flux only becomes holding force if it has a closed loop: pole piece, working gap, plunger, back through the housing wall. That is why the solenoid valve housing magnetic circuit return path matters more than the outer shape — the wall is a working component, not a bracket.
The return leg's reluctance is length over (permeability × wall area). Halve the wall area and reluctance doubles; once the leg saturates, extra current buys almost nothing. For a typical 8–12 W automotive coil, 1.2–1.8 mm of low-carbon steel keeps flux density below roughly 1.8 T; thinner walls only work with pure iron (DT4, ≈ 2.1 T) or a split flux path.
Grade choice is a force decision, not a purchasing decision:
✅ 1008/1010 carbon steel — the default, saturation ≈ 2.0 T.
✅ DT4 electrolytic iron — highest saturation headroom, for compact high-force designs.
✅ 430F stainless — for corrosive media; saturation ≈ 1.5–1.6 T with directional permeability, so expect 15–25% less force at the same wall.
✅ Magnetic anneal after forming — stamping cold work raises coercivity; critical parts are annealed at 850–900 °C. A 430F quote that never mentions anneal will drift batch to batch.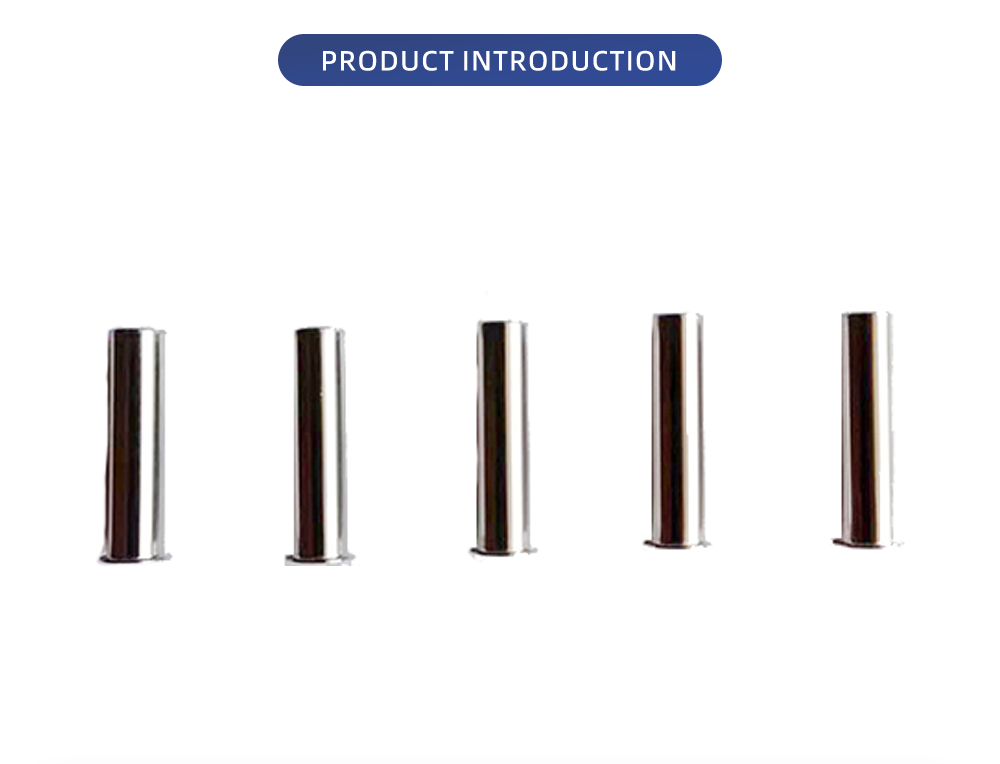
Function 2 — It sets the air gap and guides the plunger
Force in the gap falls roughly with the square of the gap: from 0.4 mm to 0.45 mm costs about 20% of the force, and at a 0.25 mm proportional design a 0.03 mm stack-up error is already 25%. The housing owns that gap through the bore depth and the seat face the pole piece presses against.
Two geometric controls dominate: seat-face squareness to the bore axis (0.02–0.03 mm) and bore-to-seat concentricity (0.03–0.05 mm TIR). Miss them and the plunger is pushed sideways — friction rises, hysteresis widens, and a proportional valve specified at 5% hysteresis starts showing 10–12% and hunting at mid-stroke.
Function 3 — It holds the pressure
The housing is often the only metal between the medium and the environment: transmission shift valves 5–25 bar, engine oil 4–10 bar, coolant 2–3 bar, brake circuits 100–180 bar. Three features seal: the O-ring groove (Ra 0.8–1.6, no spiral tool marks), the seat face (flatness ≤0.02 mm), and the wall itself.
Wall integrity is process-dependent. A deep-drawn, ironed wall has no porosity path, so the risk moves to the laser weld or braze at the flange — hence weld penetration control and post-weld leak testing. A die-cast housing is the opposite: sound skin, shrinkage porosity at thick-to-thin transitions, so vacuum casting and impregnation where needed. Either way the criterion is a number, not a visual: typically 1×10⁻³ mbar·L/s helium at 1.5× proof pressure.
Function 4 — It locates the valve and sinks the coil's heat
The pilot diameter locates the valve in the manifold bore; a flat or key sets port orientation, at 0.1 mm positional tolerance. The housing is also the coil's heat sink, moving 3–8 W into the manifold. Poor contact raises coil temperature, copper resistance climbs about 0.4% per °C, and a coil rated at 20 °C has lost roughly 20% of its ampere-turns by 120 °C — which is why the same valve can measure differently in two manifolds.
✅ Bottom line: A housing is a magnetic, hydraulic and locating component in one part — specify permeability, gap geometry and leak rate, not just dimensions.
2. Why does the housing decide whether the valve works — and why do drawings miss it?
Because the properties that decide performance — permeability after forming, wall thickness in the flux path, and seat-to-bore geometry — are invisible on a dimensional drawing, and housings are still bought as if they were drawn cups.
Solenoid valve housing vs plain drawn cup: the difference is the specification, not the shape
A drawn cup is bought on OD, ID, height and wall thickness. A housing needs all of that plus anneal state and permeability, minimum return-path wall at three sections, bore cylindricity and Ra, seat flatness, leak rate, coating, and a pull-force callout cold and hot. That is the real content of a solenoid valve housing vs plain drawn cup comparison: same envelope, different product. Buyers re-asking what does a solenoid valve housing actually do while comparing quotes are really asking which specification they are buying.
Cost follows the specification, not the geometry. A plain 30 mm drawn cup at 1.5 mm wall runs roughly $0.15–0.40 at 100k pieces per year; the same envelope as an annealed, leak-tested, coated housing with a controlled bore runs $0.8–3.5, plus progressive-die tooling at $8,000–25,000. Quotes compared on price per kilogram are comparing two different parts — the cheaper one usually reappears as an EOL pull-force failure.
What belongs on the drawing
✅ Material and anneal state — 1008/1010, DT4 or 430F, with "magnetic anneal after forming" spelled out and a permeability or pull-force acceptance attached.
✅ Minimum wall thickness in the return path, measured at three sections, not a nominal.
✅ Bore diameter, cylindricity and Ra; seat-face flatness and squareness.
✅ Proof pressure and maximum leak rate, with the test method named (helium, pressure decay, air-under-water).
✅ Coating and salt-spray hours — 480 h under-hood, 720 h chassis-adjacent.
✅ Pull force at rated current, cold and at soak temperature.How to verify before PPAP
Three checks catch most housing problems: a pull-force curve cold and hot, a helium leak test at proof pressure, and a CMM run on bore-to-seat geometry across the first 30 parts of every cavity. A flux map of the return path shows saturation years before it becomes a warranty claim. Nantong Kunda Metal Products Co., Ltd. runs all four in-house on progressive-die programs — which is why we ask for the coil's force curve before quoting a custom housing, not after the first failure.
✅ Bottom line: Two housings with identical dimensions can differ 20% in holding force; the specification, not the envelope, decides which one you get.
FAQ
Q: What does a solenoid valve housing actually do that a mounting bracket does not?
A bracket only positions the coil. The housing is the solenoid valve housing magnetic circuit return path, the air-gap fixture, the pressure wall and the manifold pilot — remove any one role and the valve loses force, repeatability or leak-tightness with a healthy coil.
Q: How much does wall thickness change holding force?
In the saturated region of the return path, dropping from 1.5 mm to 1.1 mm wall can cost 10–20% of holding force at rated current, and more current recovers none of it. Measure wall thickness at three sections of the flux path and pull-force test cold and hot.
Q: Can a stamped housing replace a machined one?
Above roughly 20,000–30,000 pieces per year, yes — a stamped-and-annealed housing with a machined seat is the standard answer, tooling at $8,000–25,000 amortized over the program; machined bodies stay right for prototypes and low volumes. The full solenoid valve housing vs plain drawn cup decision hinges on volume, gap tolerance and whether the bore itself guides the plunger.
Get a housing review before you tool it
Send a drawing and the coil's force curve — Kunda Metal returns a DFM review within 48 hours covering return-path wall thickness, anneal recommendation, gap stack-up and a factory-direct price at your annual volume. As an IATF 16949 and AS9100D certified OEM housing supplier in China, we quote bulk programs from 20,000 pieces per year and prototypes from 500. See our solenoid valve housing capabilities or a sample precision stamped housing, then contact our engineering team to start the review.
http://www.kundametal.com
Nantong Kunda Metal Products Co., Ltd. -
AuthorPosts

- You must be logged in to reply to this topic.