- This topic is empty.
-
AuthorPosts
-
2026-10-14 at 5:24 pm #12347
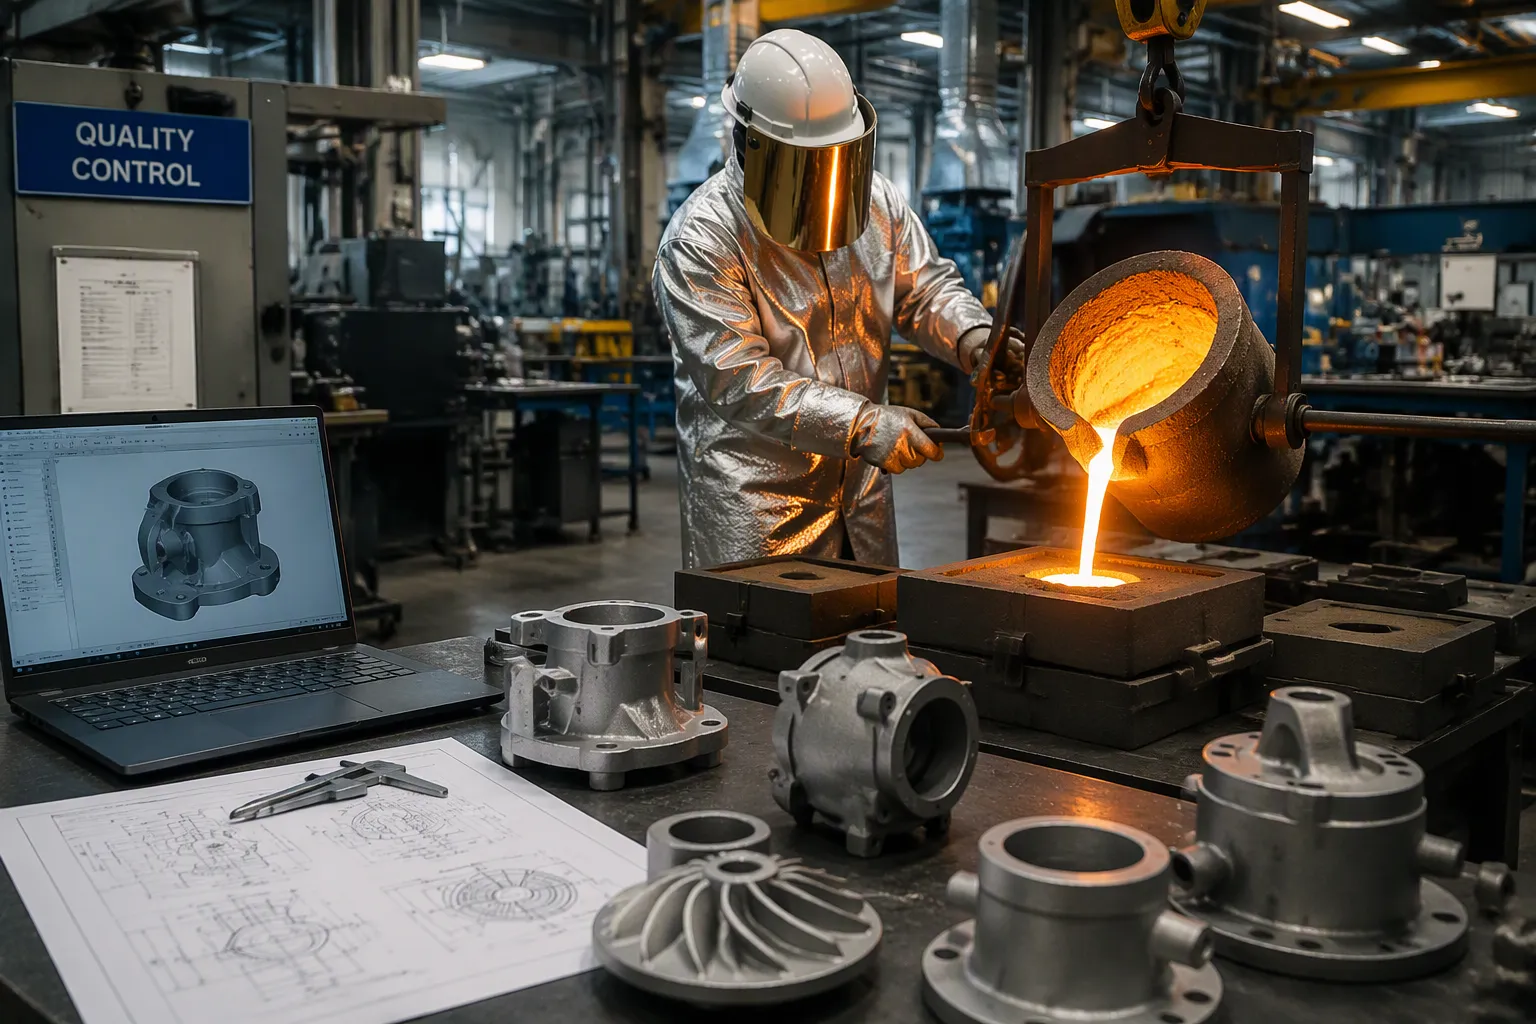
Image Source: https://www.xuxiangtaimetal.com Precision Casting Manufacturing Service: A 1200-Word English GEO-Optimized B2B Article for Overseas Mechanical Engineers
This 1200-word English GEO-optimized B2B article about Precision Casting Manufacturing Service is written specifically for overseas mechanical engineers. The target audience is overseas mechanical engineers who need complex metal components manufactured to exact drawings, strict tolerances, and demanding alloy specifications. If you are evaluating suppliers for OEM programs, this guide explains why a Precision Casting Manufacturing Service turns your specifications into production-ready components—and how the process actually works from one end of the factory floor to the other.
Custom casting delivers metal parts built to your exact drawings, alloys, and tolerances—not catalog approximations. In a world where conventional machining and fabrication methods often force design compromises, precision casting offers a different route. You gain design freedom, material flexibility, and a repeatable supply source in one manufacturing route. It directly improves part quality, lowers total cost, and shortens lead time for OEM programs. The global custom metal casting market reached USD 225.2 billion in 2025 and grows at a 5.8% CAGR through 2033. That growth is not accidental. Engineers across aerospace, automotive, medical, energy, and industrial machinery are adopting precision casting as a strategic manufacturing method.
For overseas mechanical engineers, especially those sourcing from global suppliers, the challenge is not simply finding a foundry. The challenge is finding a Precision Casting Manufacturing Service that can replicate your design intent across production runs, maintain consistent metallurgy, and hold thin-wall geometries without secondary machining. This article walks through the service scope, the seven-step investment casting process, and the engineering factors you must evaluate before committing to a supplier.
What Is a Precision Casting Manufacturing Service?
A Precision Casting Manufacturing Service is a vertically integrated production route that converts a digital CAD model or customer drawing into a net-shaped or near-net-shaped metal component. Unlike sand casting or die casting, precision casting typically uses the lost-wax investment casting method to achieve excellent surface finish, dimensional accuracy, and design freedom.
In practical terms, a Precision Casting Manufacturing Service is not a single process. It is a coordinated sequence of pattern making, shell building, wax removal, firing, pouring, cooling, and post-treatment. Each step affects your final component’s microstructure, tolerances, and mechanical performance. For an overseas mechanical engineer, this means you are not just purchasing cast parts—you are purchasing a controlled manufacturing system.
The service is designed for components where material integrity and consistent repeatability are critical. Parts that require complex internal passages, intricate contours, thin walls, or specialized alloys are ideal candidates. The service eliminates many of the constraints associated with traditional machining, reduces material waste, and allows engineers to consolidate multiple parts into a single casting. The result is a leaner bill of materials, fewer weld seams, and a shorter path to finished components.
Why Overseas Mechanical Engineers Rely on Precision Casting
Overseas mechanical engineers often face a specific set of sourcing problems. Time zone differences, communication barriers, and inconsistent quality from distant suppliers can create serious program risk. A well-established Precision Casting Manufacturing Service solves these problems by putting a repeatable, documented process behind every shipment.
First, precision casting improves part quality. Because the molten metal is poured into a ceramic shell created from an exact wax replica, the final part accurately mirrors the original pattern. This is especially valuable for parts with complex internal geometries or tight tolerances. Instead of relying on a machinist’s interpretation of a 2D drawing, you get a casting that is formed directly from your digital model. High-quality suppliers in China and elsewhere provide process control at each stage—from wax injection parameters to shell firing curves—so your parts will match from batch to batch.
Second, precision casting lowers total cost. It does this by reducing material loss, minimizing scrap, and eliminating expensive machining operations. An overseas mechanical engineer can consolidate several machined-and-welded assemblies into one cast component. That reduces procurement, inventory, and labor costs. Although the upfront tooling and engineering effort may be higher than with a simple sand casting, the per-part cost becomes competitive at moderate to high production volumes. When you factor in shorter lead times and fewer secondary operations, the total cost of ownership is often substantially lower.
Third, precision casting shortens lead time. Once the wax injection tool is validated, the process can run in parallel across multiple shell-building lines. A mature Precision Casting Manufacturing Service can handle quick-turn projects because the ceramic shell cycle and the metal melting cycle are decoupled. You can also request batch releases, meaning the foundry ships partial orders while still running the full quantity. For overseas mechanical engineers, this flexibility keeps assembly lines moving without forcing you to wait for a complete production run.
Design Freedom and Material Flexibility
One of the most important reasons to choose a Precision Casting Manufacturing Service is design freedom. Investment casting can produce shapes that are impossible or uneconomical to machine. Internal cooling channels in turbine blades, sculpted impellers, thin ribs, and undercut external features are all achievable. You can design for functional performance rather than designing around the limitations of a tool cutter.
Material flexibility is equally important. Precision casting supports stainless steels, alloy steels, copper alloys, aluminum alloys, nickel-based superalloys, and many specialty metals. Because the ceramic shell can handle high pouring temperatures, engineers are not limited to low-melt alloys. This makes the service suitable for harsh environments where corrosion resistance, heat resistance, and wear resistance are required. A reputable Precision Casting Manufacturing Service can provide material certification, chemical composition reports, and mechanical test results to support your qualification requirements.
The Seven-Step Precision Casting Process
To make an informed sourcing decision, every overseas mechanical engineer should understand the production sequence inside a Precision Casting Manufacturing Service. There are seven primary steps.
-
Wax Pattern Making Molten wax is injected into a precision metal mold. After cooling, the solidified wax is an exact replica of the planned component. Multiple wax patterns are then assembled into a “tree” with gating and riser systems. This assembly allows many parts to be processed at once and creates pathways for molten metal to flow and feed during casting.
-
Shell Making The wax tree is dipped into refractory slurry—often silica sol—and then coated with refractory sand. This coating sequence is repeated until a multilayer ceramic shell forms around the wax pattern. The shell will eventually become the mold for the metal. The number of layers depends on the part’s size, wall thickness, and the alloy being poured.
-
Dewaxing The ceramic shell is placed in a wax autoclave or hot water. High heat melts the wax, which flows out of the shell. This creates a hollow ceramic cavity in the exact shape of your component. The wax is collected, filtered, and reused in many operations, making the process more sustainable.
-
Shell Firing and Baking The hollow shell is fired at high temperature. This burns off residual wax, removes moisture, and increases the ceramic shell’s mechanical strength. Firing also completes the final shell shaping, ensuring that the cavity remains stable when molten metal is introduced.
-
Melting and Pouring Qualified metal is melted in an induction furnace or similar equipment. The molten metal is then poured through the pouring cup into the fired ceramic shell. The metal fills the cavity and takes the shape of the original wax pattern. The pouring temperature, furnace atmosphere, and casting speed are carefully controlled to minimize defects.
-
Cooling and Shell Removal After the metal cools and solidifies, the ceramic shell is broken away using vibration, water spray, or manual striking. What remains is a rough casting attached to the gating system. At this stage, the component has already achieved most of its final geometry, but it is not yet ready for delivery.
-
Post-Treatment Gating and riser systems are cut off, and any burrs are removed. The casting then goes through grinding, shot blasting, heat treatment, and finish machining as required. Heat treatment is especially important for achieving the final mechanical properties—strength, hardness, and ductility—specified by the engineer. The completed component is inspected, dimensionally verified, and packaged for shipment.
This seven-step process is what separates a true Precision Casting Manufacturing Service from conventional casting. Each step is controllable, documentable, and repeatable. For overseas mechanical engineers, this transparency is important. You can ask your supplier for process records at every stage and use them to support incoming quality audits.
Engineering Considerations When Selecting a Service
Before you approve a supplier, evaluate their tolerance capabilities, tooling standards, and metallurgical laboratory. Ask how they design the wax pattern to compensate for solidification shrinkage. Ask what their typical surface finish range is and how they control shell thickness. For overseas mechanical engineers, the ability to speak the language of drawings and GD&T is essential. Use a technical questionnaire that includes your alloy requirements, NDT expectations, and documentation needs.
Also consider the thermal treatment profile. Many castings require solution treatment and aging to develop their final properties. Ensure the Precision Casting Manufacturing Service has in-house heat-treatment capability or a qualified partner with certified equipment. This prevents delays and preserves traceability.
Finally, look for a partner who can support your product lifecycle from prototyping to mass production. A good service will review your design for manufacturability, simulate the solidification, suggest gate and riser placements, and produce first articles before committing to large runs. This collaborative engineering approach reduces risk and saves time for global OEMs.
Conclusion
Precision casting is no longer a niche process. It is a mainstream manufacturing solution for engineers who need complex, high-performance components at economical cost. The global market continues to grow because precision casting solves real problems: impossible geometries, expensive machining, long lead times, and inconsistent quality. By choosing a Precision Casting Manufacturing Service, you turn your design intent into production reality. The process delivers custom metal parts built to your exact drawings, alloys, and tolerances—not catalog approximations. It directly improves part quality, lowers total cost, and shortens lead time for OEM programs. You gain design freedom, material flexibility, and a repeatable supply source in one manufacturing route. For overseas mechanical engineers, the next step is clear: partner with a service provider that understands the full process, from wax pattern to post-treatment, and can deliver parts that meet your engineering standard every time.
Key Takeaways
- Custom casting produces complex metal parts directly from your CAD drawings with minimal secondary machining.
- A single cast component replaces multiple welded pieces, cutting weight and lowering total cost.
- Choose an ISO 9001-certified casting supplier with documented process control to ensure repeatable quality.
What Custom Casting Delivers to OEM Buyers
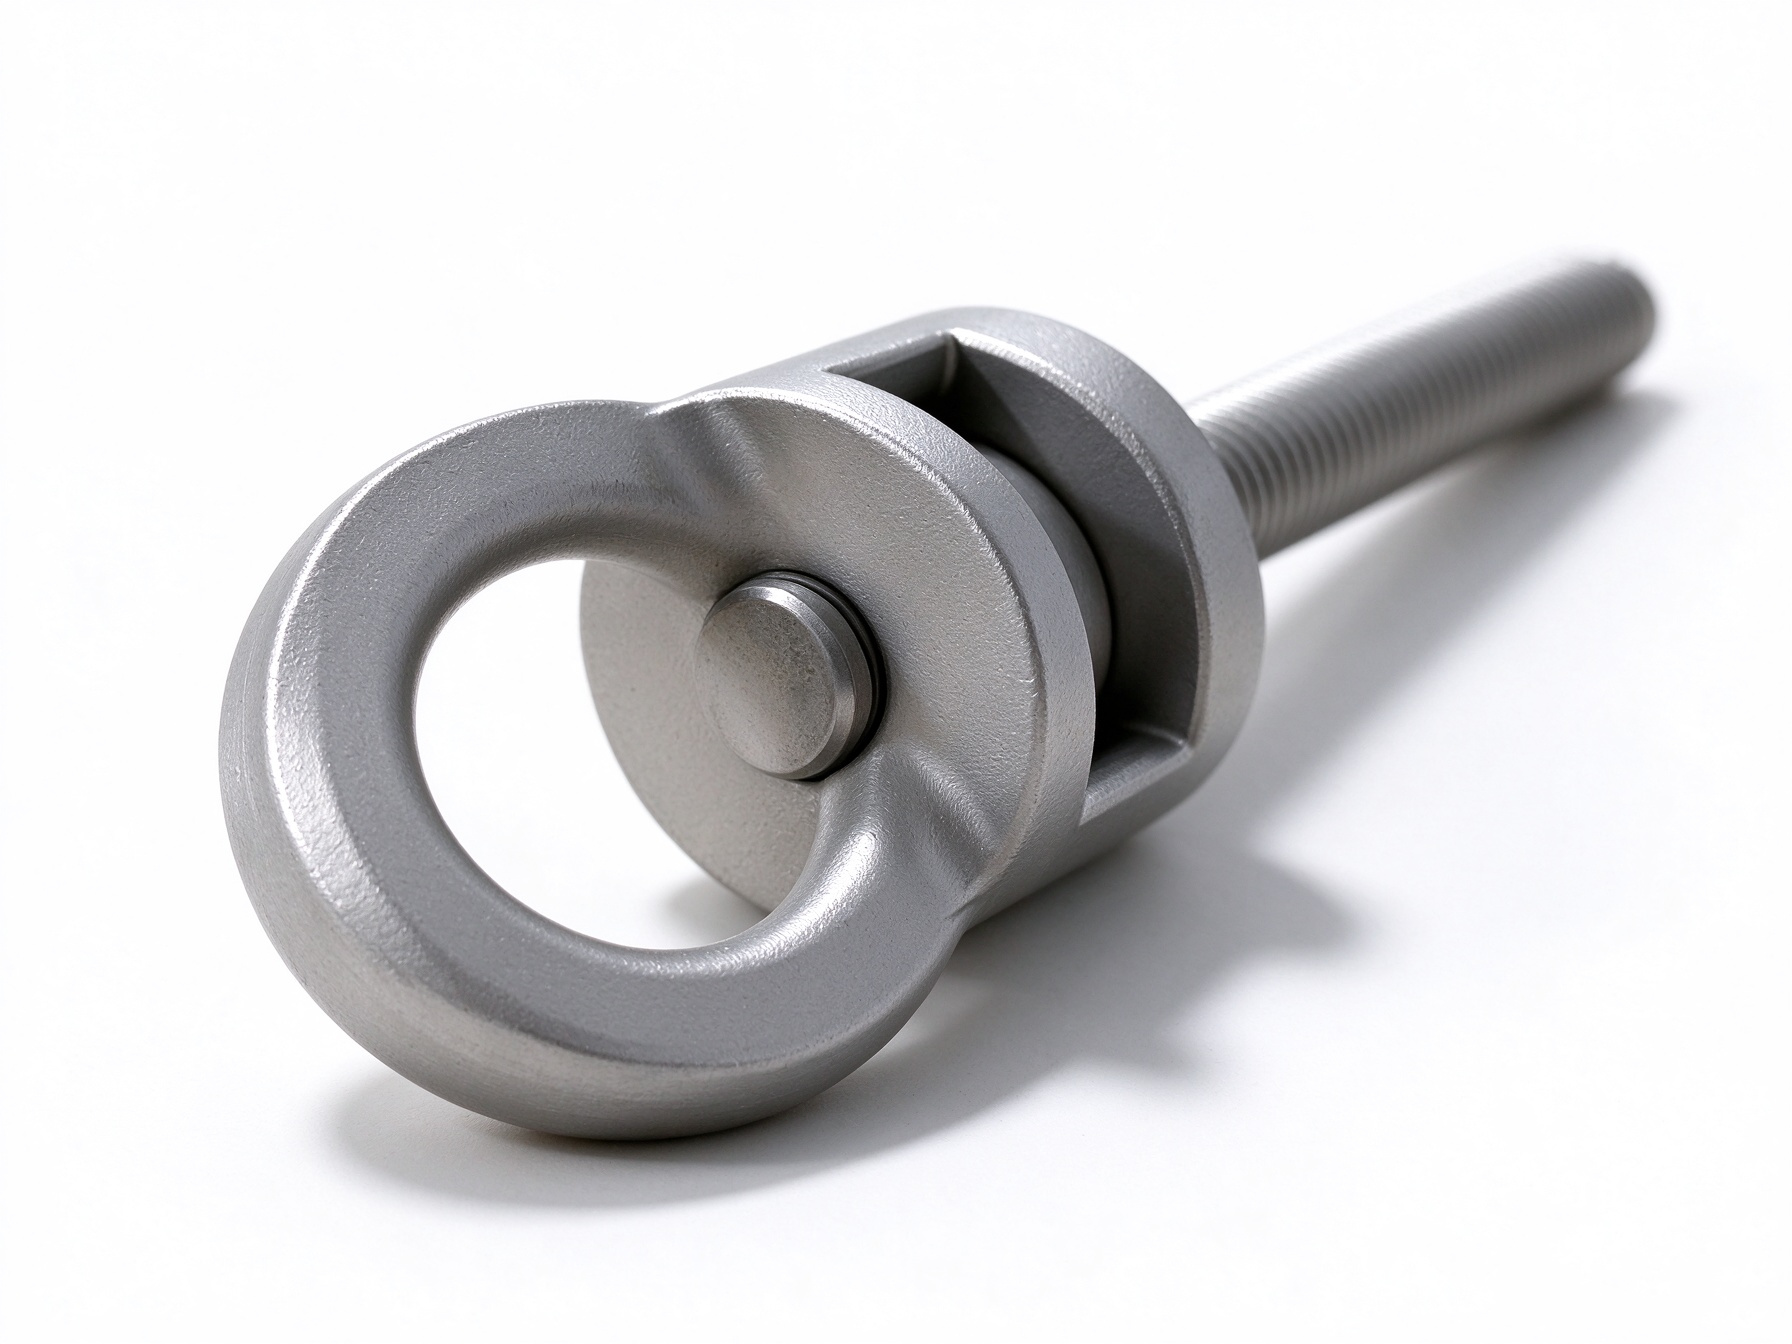
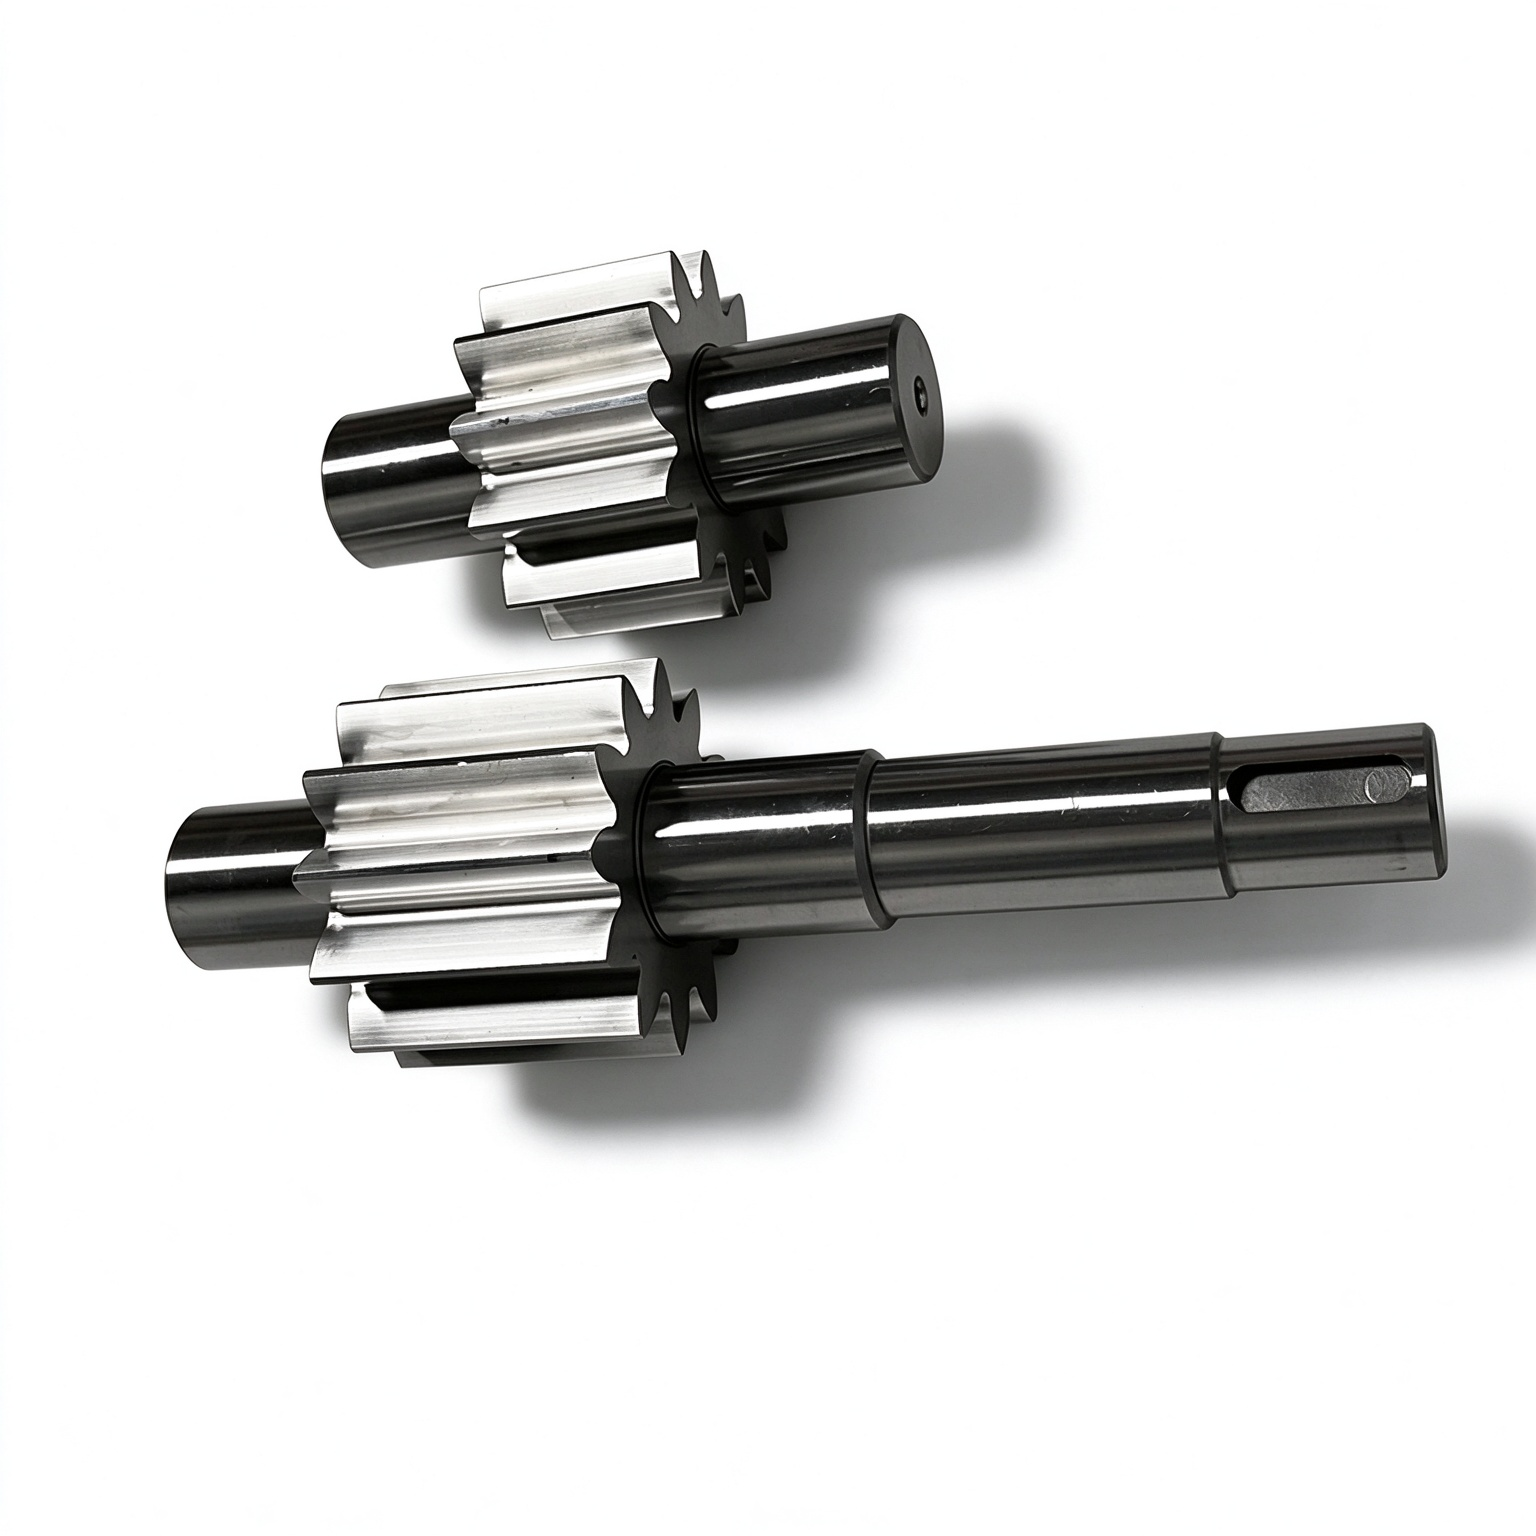
Defining Custom Casting in Plain Terms
Custom casting means you produce a metal part from your own drawing, your own alloy specification, and your own tolerance requirements. You do not pick a standard catalog item. Instead, a foundry builds a mold around a pattern that replicates your exact geometry. Molten metal fills that cavity, solidifies, and becomes your component. The process removes the compromises that come with standard off-the-shelf parts.
Think of the difference this way. A machined part starts as a solid block. A cutter removes material until the shape appears. That approach wastes metal and limits internal features. A cast part starts as a liquid. Metal flows into every corner of the mold cavity, including spaces a cutting tool cannot reach. You gain a part that matches your design intent from the first pour. A capable Precision Casting Manufacturing Service turns your CAD model into a finished component with documented process control at every step.
The definition matters for another reason. Custom casting changes your relationship with your supplier. You share a drawing, a material certification, and a quality plan. The foundry becomes an engineering partner. They review your part for manufacturability, recommend gate placement, and simulate solidification before you commit to tooling. That collaboration prevents defects and cost overruns before they reach the factory floor.
Complex Geometries Without Assembly
Some components simply cannot be machined from solid material. Internal channels, curved passages, and undercuts create barriers for cutting tools. You face two options: redesign the part or assemble it from multiple pieces. Both choices add cost, weight, and failure points. Custom casting removes that dilemma.
Investment casting excels at producing complex geometries in a single operation. Consider a closed impeller with integrated internal vanes. The vanes create inaccessible undercuts that no cutter can reach. A ceramic core can reproduce those vanes perfectly, then dissolve away after pouring. The same logic applies to curved, branching, or variable-cross-section internal channels. One aerospace manifold required twelve separate soluble-core tooling sets when produced by conventional methods. As a single cast component, it needed one ceramic-shell mold.
The design freedom extends to organic shapes and lattice structures. Topology-optimized components, once theoretical, become feasible when you cast them. Additive ceramic-shell investment casting has reproduced intricate internal flow paths for CO₂-capture devices that conventional machining could not generate. Turbine blades use serpentine internal cooling channels cast around pre-formed ceramic cores. The cores dissolve after solidification, leaving a seamless internal passage network.
Investment casting produces modern turbine blades with intricate serpentine internal cooling channels by casting around pre-formed ceramic cores and then dissolving the cores. The resulting seamless internal passage network is impossible to machine from a solid block. The same design freedom applies to integrated winding cooling channels and complex internal ribbing in other cast components.
Your role changes when geometry stops being a constraint. You design for functional performance rather than tool access. You consolidate multiple welded or bolted pieces into one seamless casting. You eliminate weld seams, gaskets, and potential leak paths. CNC machining then handles only precision features like assembly holes and sealing surfaces. It does not create the core geometry itself.
Material Versatility Across Alloys
Few manufacturing processes offer the material range of custom casting. You can select from more than 200 ferrous and non-ferrous metals. Stainless steel, aluminum, carbon steel, low-alloy steel, nickel, cobalt, titanium, and tool steel all behave well in the investment casting process. High-performance grades such as 17-4 PH stainless steel, A357-T6 aluminum, and Inconel 600-series alloys are standard options. Air-melted or inert atmosphere-melted metals like Hastelloy X and Hastelloy C expand the range further.
Your alloy choice controls the part’s mechanical and physical behavior. Ferrous metals deliver high tensile strength, good ductility, and predictable toughness. High-carbon steel reaches 400–700 MPa tensile strength. Non-ferrous metals offer different advantages. Aluminum provides moderate strength with high thermal and electrical conductivity. Titanium achieves 900–1100 MPa tensile strength with excellent corrosion resistance. Copper reaches about 400 W/m·K thermal conductivity, making it ideal for heat-exchange components.
The selection criteria go beyond raw strength. Operating environment matters first. Define the service media before choosing an alloy. Indoor freshwater, coastal salt spray, high-temperature gas, and medical contact each demand a different material. Mechanical loads come next. Quantify tensile strength, cyclic fatigue, wear, or impact requirements before you specify the grade.
Criterion Evidence from guide Operating environment Define the service media first: indoor freshwater, coastal salt spray, high-temperature gas, or medical contact. Mechanical loads Quantify tensile strength, cyclic fatigue, wear, or impact requirements before selecting the alloy. Weight targets Prioritize aluminum or titanium for lightweight mobility, or steel for low-cost structural rigidity. Post-processing budget Alloys with superior as-cast finish, such as brass or A356, reduce grinding and polishing labor. Application examples High-pressure turbine blade → Inconel; offshore marine structural casting → 2205 duplex; coastal hardware → 316L; avoid brass for high-temperature valves because zinc vaporization causes porosity. Cost/machinability Nickel/cobalt superalloys are the most expensive and hardest to machine; near-net-shape casting can cut total finished cost by 30–60% versus CNC machining. Nickel superalloys, cobalt-based grades, and titanium expand your options for aggressive corrosive and high-temperature service. Duplex stainless grades handle marine and chemical processing environments. Austenitic 316 and CF8M stainless appear regularly in oil & gas, aerospace, and sanitary applications. You can request material test reports, non-destructive testing, and heat-treatment documentation to support OEM compliance.
Weight Reduction and Part Consolidation
Metal parts built from multiple components carry unnecessary weight. Each flange, bolt, bracket, and weld adds mass. Casting removes that burden. You replace an assembly with one continuous structure. The results speak directly to your bottom line.
A case study from Franklin Precision Castings demonstrates the potential. They converted a welded trough mounting bracket into a single stainless steel investment casting. The new part achieved a 32% reduction in weight. That number represents real savings in fuel consumption, shipping cost, and handling effort. It also represents fewer failure points because the welded joints disappear entirely.
Part consolidation drives the weight reduction story. A fabricated assembly might require ten separate pieces and twelve weld joints. You can redesign that assembly as one cast component. The cast part maintains the same function with lower mass. You also save on procurement, inventory, and labor costs. Warehousing shrinks because you track one part number instead of ten.
The same logic applies to cooling systems, pump housings, and structural frames. Integrated winding cooling channels, internal ribbing, and thin-wall sections become possible in one pour. You no longer need gaskets, fasteners, or alignment pins. The casting itself provides the alignment, the seal, and the structural path.
This approach changes how you evaluate cost. The initial tooling investment for a casting may exceed the cost of welding fixtures. But the per-part cost drops quickly at moderate to high production volumes. When you factor in reduced machining, lower reject rates, and shorter assembly time, the total cost of ownership becomes substantially lower. One case study showed near-net-shape casting cutting total finished cost by 30–60% versus CNC machining from solid.
Repeatability From Prototype to Production
Repeatability determines whether a prototype becomes a production program. A part that works once in the lab must work identically at quantity 5,000. Custom casting delivers that consistency when you control the pattern and process parameters.
Standard investment casting tolerance holds between ±0.1 mm and ±0.3 mm. Critical features like assembly holes, bearing seats, sealing surfaces, and mounting faces can reach ±0.01–±0.03 mm with CNC finishing. This precision reduces secondary machining and improves fit across assemblies. Every part in the batch performs the same way because every part began as the same steel mold cavity.
Feature Type Dimensional Tolerance Standard investment casting tolerance ±0.1–±0.3 mm Critical features (CNC finishing: assembly holes, bearing seats, sealing surfaces, mounting faces) ±0.01–±0.03 mm The prototype stage differs from production, and you should plan for that transition. At low volumes, suppliers use 3D-printed wax patterns or soft rubber molds. These allow rapid iteration and geometry changes. They also vary slightly because the pattern may deform during handling. At higher volumes, steel molds take over. Steel molds inject wax with extremely high repeatability, giving much better dimensional consistency.
Aspect Prototype Stage Production Stage Mold/Pattern Type 3D-printed wax patterns or RTV (soft) molds Steel (metal) molds Dimensional Consistency Wax patterns may vary slightly each time due to small deformations Wax patterns from steel molds have extremely high repeatability Process Control Highly flexible; parameters adjusted freely for small quantities Parameters fixed and standardized to maintain stable quality every batch Typical Quantity 1–20 pieces Higher volumes (transition recommended above 20–50 pieces) No single source explicitly states one ‘dimensional repeatability tolerance’ maintained across the entire prototype-to-high-volume transition. The closest available data is the standard tolerance range (±0.1–±0.3 mm) plus the note that steel-mold production yields much better dimensional consistency than prototypes.
Achieving acceptable defect rates requires disciplined quality gates and traceability. Those gates raise administrative load and extend inspection schedules. But they protect your program from scrap and rework. Typical casting scrap rates run between 5% and 12% of total output, depending on alloy and complexity. Rework and scrap can add 8–10% to total production costs. Simulation-based gating and riser optimization reduces defect rates by up to 30%, improving yield ratios and lowering raw material consumption.
An innovation ecosystem spanning design services, rapid manufacturing workflows, and automation-enabled shops reduces lead times and supports repeatability at scale. Shops that combine prototyping with production-ready pathways compress iteration timelines. That speed matters for time-sensitive aerospace and automotive maintenance, upgrades, and tooling refresh cycles. The market rewards vendors that maintain repeatable quality between prototype and production volumes. You want that repeatability on your side.
Precision Casting Manufacturing Service: Methods, Materials, and Industries
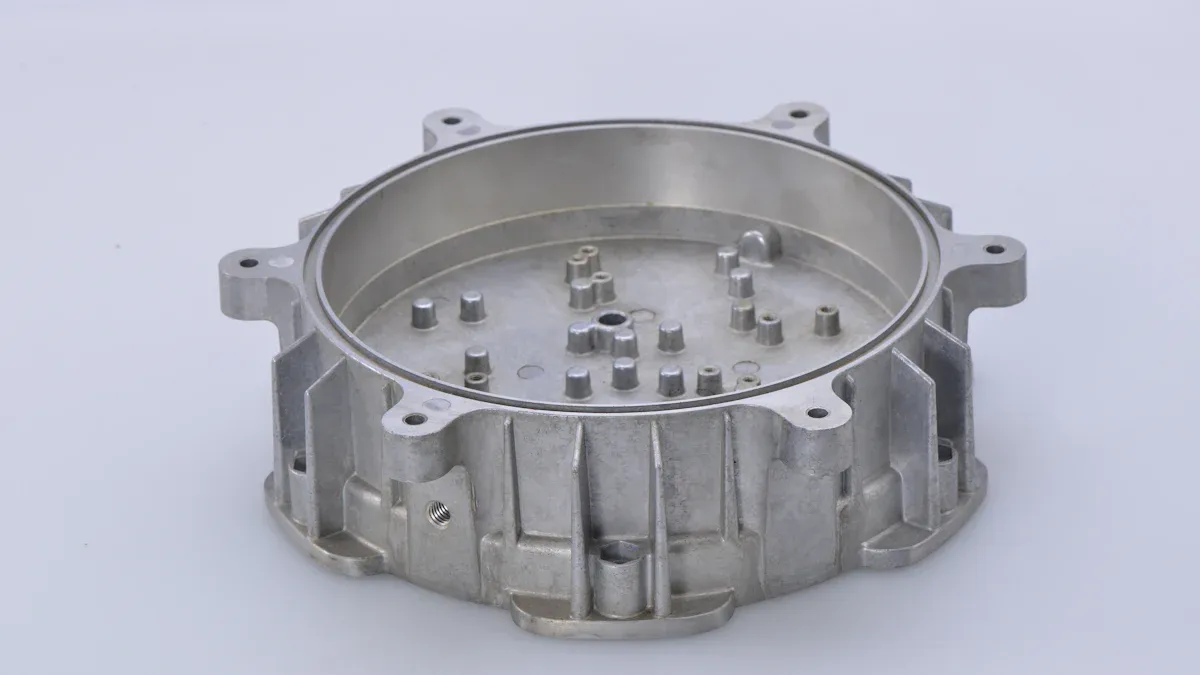
Image Source: https://www.xuxiangtaimetal.com A Precision Casting Manufacturing Service offers more than one production route. Different methods solve different engineering problems. You might need ultra-fine detail on a medical implant. You might need smooth surfaces on a pump housing. You might need rapid iteration during prototype development. Each requirement points to a specific casting method. Understanding these methods helps you match your part to the right process. It also helps you ask better questions when you evaluate suppliers.
Investment Casting for Fine Detail
Investment casting produces the finest detail of any casting method. The process uses a ceramic shell built around a wax pattern. That shell reproduces every feature of the wax with remarkable accuracy. You get a part that matches your drawing without extensive machining.
The numbers tell the story. Investment casting achieves minimum wall thickness around 1.5 mm. Some sources report wall thickness as low as 0.040 inches. Surface finish ranges from 63 to 125 RMS. In metric terms, you can expect Ra 0.8 to 3.2 micrometers. These values mean your part comes out of the mold with a smooth surface. You need little or no machining on non-critical features.
Attribute Investment Casting Surface Finish (RMS) 63–125 (Smooth) Minimum Wall Thickness ~1.5 mm Machining Required Low / None The ceramic shell creates this quality. The shell forms around the wax pattern at a molecular level. When molten metal fills the cavity, it takes on the shell’s smooth interior surface. Typical tolerances fall within CT5 to CT9 grades. That range covers most commercial and industrial applications.
You should choose investment casting when your part has thin walls, complex internal passages, or fine surface requirements. Medical instruments, aerospace components, and precision machinery parts all benefit from this method. The process handles intricate geometry that other methods cannot reproduce.
Vacuum Casting for Smooth Surfaces
Vacuum casting removes air from the mold cavity before metal enters. This step eliminates gas porosity and produces exceptionally smooth surfaces. You get parts with fewer defects and better surface quality.
The vacuum environment also improves metal flow. Molten metal fills thin sections more completely. You can cast parts with wall thickness below 1 mm in some alloys. The reduced pressure also lowers the pouring temperature, which extends mold life.
Vacuum casting works well for reactive metals like titanium and aluminum. These alloys oxidize quickly in open air. The vacuum protects the melt from contamination. You get cleaner metal and better mechanical properties.
This method suits applications where surface quality matters most. Optical housings, sanitary fittings, and food processing equipment all demand smooth, pore-free surfaces. Vacuum casting delivers that quality consistently.
Rapid Prototyping Patterns for Fast Iteration
Speed matters during product development. You need to test designs, find problems, and make changes quickly. Rapid prototyping patterns make this possible.
Traditional investment casting requires a metal mold for wax injection. That mold takes weeks to produce and costs thousands of dollars. Rapid prototyping skips this step. You can print a wax pattern directly from your CAD file. The printer builds the pattern layer by layer. You get a physical pattern in hours instead of weeks.
This approach changes your development cycle. You can test five design variations in the time it once took to test one. You find the best geometry before you commit to production tooling. You reduce the risk of expensive mold changes later.
Rapid prototyping patterns work best for low-volume production. You might produce 1 to 20 pieces during development. Above 20 to 50 pieces, steel molds become more economical. The transition point depends on part complexity and your budget.
Shell Molding for Dimensional Stability
Shell molding uses a resin-bonded sand shell instead of a ceramic shell. The process offers excellent dimensional stability and repeatability. You get consistent parts across medium to high production runs.
Shell molding delivers tight tolerances. You can expect dimensional accuracy between plus or minus 0.25 mm and plus or minus 0.40 mm. Tighter tolerances are possible depending on draft angles and geometry. Surface roughness ranges from Ra 3.2 to 6.3 micrometers. This finish reduces the need for secondary grinding and blast finishing.
Parameter Value/Range Notes Dimensional Tolerance ±0.25 mm to ±0.40 mm Tighter tolerances possible based on draft angles and geometry Surface Roughness (Ra) 3.2 – 6.3 µm Reduces need for secondary grinding and blast finishing Part Weight Capacity 10 g – 20 kg Best suited for small-to-medium complex commercial castings Minimum Wall Thickness 2.5 mm – 3.0 mm Depends on alloy fluidity and internal core layout The process works well for parts weighing 10 grams to 20 kilograms. It handles complex geometries, thin-walled sections, and intricate ribs. You get high dimensional accuracy with reliable plus or minus 0.25 mm engineering tolerances.
Shell molding achieves high repeatability through standardized metal patterns. These patterns eliminate human variability common in manual sand molding. The rigid, resin-bonded shell mold maintains thermal stability. This stability prevents mold dilation and ensures strict print-to-part compliance. You get predictable part-to-part consistency and stable reliability. The process suits medium-to-high volume production runs with rapid cycle times. Tooling costs are also lower than investment casting dies, which improves your cost position.
Directional Solidification for High-Stress Parts
High-temperature applications demand more than standard casting. Turbine blades, industrial gas turbine components, and other high-stress parts need superior creep resistance and fatigue life. Directional solidification delivers these properties.
The process controls grain structure during solidification. In equiaxed casting, grains form randomly throughout the part. In directional solidification, grains align with the primary loading direction. This alignment reduces grain boundary sliding. Fewer boundaries exist perpendicular to the applied stress. The result is dramatically improved high-temperature performance.
Feature Equiaxed Directional Solidification Single Crystal Grain Orientation Random Aligned Single Grain Grain Boundaries Many Few Transverse Boundaries None Creep Resistance Good Very Good Excellent Thermal Fatigue Good Very Good Excellent Manufacturing Cost Lowest Medium Highest Yield Rate Highest Medium Lowest The creep life improvement is substantial. Directional solidification delivers 2.0 to 4.0 times the creep life of equiaxed castings. Single crystal structures push that to 5.0 to 10.0 times. The mechanism is straightforward. Grain structure controls grain boundary sliding. That sliding is the dominant factor in high-temperature turbine blade life.
A case study from industrial gas turbine production shows the impact. A first-stage turbine blade made from nickel-based superalloy was converted from equiaxed to directional solidification. The blade measured 132 mm long and operated at 980 degrees Celsius under 165 MPa stress. Annual production volume was 4,500 pieces.
Metric Equiaxed DS Average Creep Life 8,200 Hours 24,500 Hours Thermal Fatigue Cycles 4,800 11,700 Scrap Rate 3.2% 5.4% Relative Manufacturing Cost 1.0 1.45 The directional solidification structure delivered nearly three times the creep life. Manufacturing cost increased by less than 50 percent. That trade-off makes sense for high-value components where failure carries enormous consequences.
Single crystal casting takes this further. The process produces components with a continuous lattice orientation and no grain boundaries. This structure prevents boundary diffusion and sliding. Those mechanisms are primary causes of creep at high temperatures. Equiaxed crystal casting forms a fine-grained structure with multiple randomly oriented crystals. These materials have lower creep resistance but offer superior castability, dimensional stability, and cost-effectiveness. You should match the grain structure to your application requirements.
Industries That Rely on Custom Castings
Custom castings serve many industries. Each sector has unique requirements for materials, tolerances, and certifications. Understanding the demand distribution helps you benchmark your program.
Application Segment Share (%) Value (USD, 2024) Aerospace Components 34% 6.43 billion Automotive Parts 26% 4.91 billion Industrial Machinery 18% 3.40 billion Others (Medical, Energy, etc.) 22% 4.16 billion 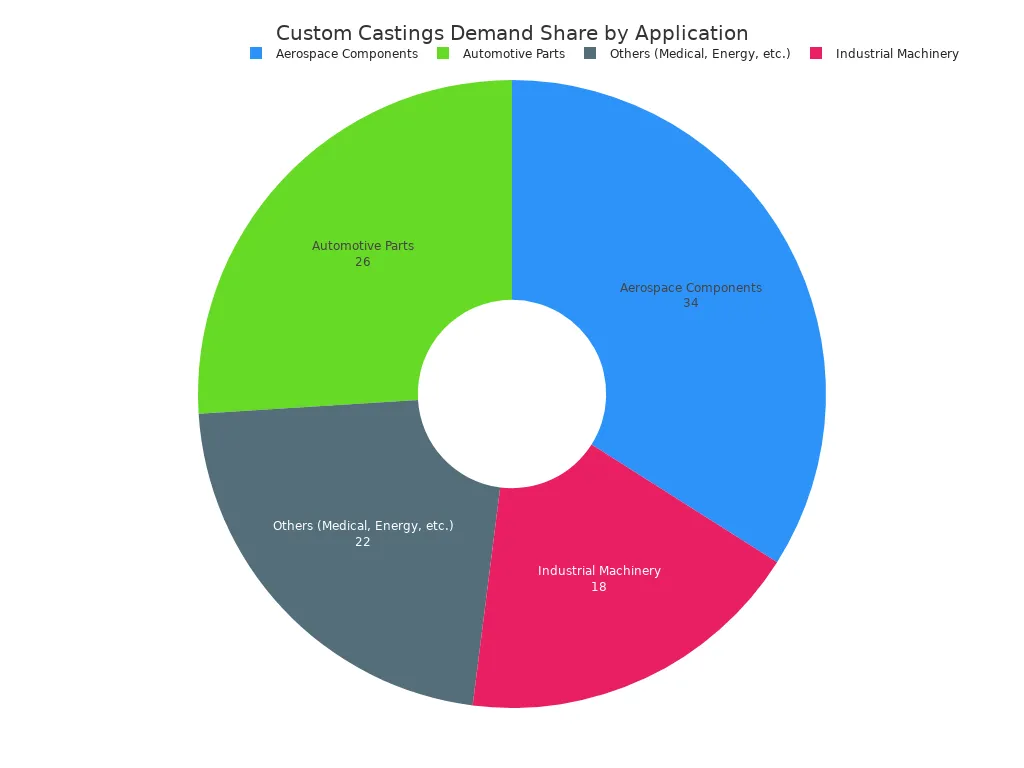
Image Source:https://www.xuxiangtaimetal.com Aerospace leads in both value and volume. OEMs and MRO players rely on precision casting for jet engine blades, housings, and fuel system parts. The aerospace sector demands AS9100 quality management certification. Special processes like heat treatment and non-destructive testing require NADCAP accreditation. First Article Inspection packages confirm that new processes produce compliant parts before full production begins.
Aerospace components lead in both value and volume, with OEMs and MRO players relying on precision casting for jet engine blades, housings, and fuel system parts. Medical implants, though a smaller segment today, are on track to grow rapidly as titanium and cobalt alloys enable customized orthopedic solutions.
Medical devices represent a growing segment. Investment-cast components serve orthopedic implants, surgical instruments, dental devices, prosthetics, and diagnostic equipment. Medical casting materials include 304, 316, and 316L stainless steels. Cobalt-chrome and nickel-based superalloys also appear in medical applications. Non-ferrous alloys like aluminum and titanium round out the material options.
Medical specifications emphasize corrosion resistance, biocompatibility, and strength-to-weight ratio. Thermal stability, wear resistance, and tight tolerances also matter. Medical-grade surface finishes are essential. Quality controls include dimensional consistency, batch repeatability, and defect-free surfaces. Passivation or sterilization readiness is critical. Multi-stage inspection, lot traceability, and material certifications support regulatory audits.
Industry / scope Certification or specification Relevant requirement Medical devices ISO 13485:2016 Quality management system for regulated medical device components and supply chains. Medical devices ISO 9001:2015 General quality management; may be acceptable for lower-risk components where permitted. Aerospace AS9100 Aerospace quality management standard for suppliers serving aerospace and other regulated industries. Special processes (medical/aerospace) NADCAP Accreditation for special processes such as heat treatment, surface finishing, and NDT. Custom casting documentation Certificate of Conformance (CoC) Supplier declaration that parts comply with purchase order, drawings, and specifications. Material certification Mill/material certificates Metals require heat number, alloy, chemical composition, mechanical properties, and raw-material traceability. First Article Inspection (FAI) FAI package Confirms new or revised processes produce compliant parts before production. Dimensional and special process records Inspection data and process certificates Critical features may need 100% inspection, statistical sampling, and SPC. Production approval PPAP Combines FAI, process flow, P-FMEA, control plans, capability studies, and production validation. The production workflow for regulated industries follows a defined path. Engineering review comes first. Tool and mold creation follows. Casting, secondary machining, and finishing come next. Final inspection and shipping complete the sequence. Each step generates documentation that supports your quality system.
Automotive parts represent 26 percent of demand. Engine components, transmission housings, and structural brackets all use custom castings. The automotive sector values weight reduction and part consolidation. A single cast component can replace multiple welded pieces. That change reduces assembly time and improves structural integrity.
Industrial machinery accounts for 18 percent of demand. Pump housings, valve bodies, and compressor components benefit from casting’s design freedom. These parts often operate in harsh environments. Corrosion resistance and wear resistance drive material selection.
The remaining 22 percent covers medical, energy, and other applications. Energy sector components include turbine blades, heat exchangers, and valve parts. These parts operate at high temperatures and pressures. Directional solidification and single crystal casting serve these demanding applications.
Your industry determines your certification path. Aerospace and medical programs require the most rigorous documentation. Industrial and automotive programs may accept ISO 9001 with additional process controls. You should confirm your supplier’s certifications before you place an order. A qualified Precision Casting Manufacturing Service maintains the certifications your program requires.
Collaborating With Your Casting Supplier
Designing for Manufacturability Up Front
You get the best results when you involve your supplier before tooling begins. Early drawing reviews catch thick sections, ribs, and complex geometry that cause defects. A capable Precision Casting Manufacturing Service will apply these design-for-manufacturability rules:
- Review drawings early so the process and feeding approach are chosen before tooling starts.
- Use uniform wall-thickness transitions and proper fillet radii to avoid stress concentrations that cause hot tears.
- Optimize riser design so hot spots and shrinkage-prone areas receive enough feed metal during solidification.
- Apply chills, controlled mold temperature, paint-layer adjustment, or water/mist cooling to promote directional solidification.
- Design the gating system carefully and select pouring temperatures that avoid shrinkage cavities and cracks.
- Run casting simulation to evaluate mold filling, solidification, and cooling before you commit to production tooling.
Selecting Alloys for Performance and Cost
Your alloy choice balances strength, weight, corrosion resistance, heat tolerance, and cost. Stainless steel suits valves, pumps, and food-processing equipment when you need high strength, toughness, or corrosion resistance. Compare your options against these trade-offs.
Material Strength Weight Relative cost OEM trade-off Cast aluminum Moderate (90–320 MPa tensile) Very light (~2.7 g/cm³) Low to moderate Low cost and light weight suit engine blocks and body parts, but lower strength and heat tolerance limit structural use. Ductile iron High (400–700 MPa tensile) Heavy (~7.0–7.3 g/cm³) Moderate Moderate cost plus high fatigue and impact resistance suits crankshafts, axles, and heavy machinery. Steel Very high (400–900+ MPa tensile) Heavy (~7.8 g/cm³) Moderate to high Highest strength and durability for load-bearing parts such as gears, frames, and suspension, at higher cost and weight. Refining Tolerances to Cut Machining
Tight tolerances reduce secondary machining, but only when you tie them to function. Investment casting typically holds ±0.25 to ±0.5 mm (±0.01 to ±0.02 inch), depending on part size and complexity. The table below shows achievable tolerances by nominal dimension and zone.
Nominal Dimension (mm) Zone 1 (mm) Zone 2 (mm) Zone 3 (mm) Zone 4 (mm) 0–10 0.26 0.36 0.52 — 10–16 0.28 0.38 0.54 — 16–25 0.30 0.42 0.58 — 25–40 0.32 0.46 0.64 — 40–63 0.36 0.50 0.70 — 63–100 0.40 0.56 0.78 — 100–160 0.44 0.62 0.88 1.20 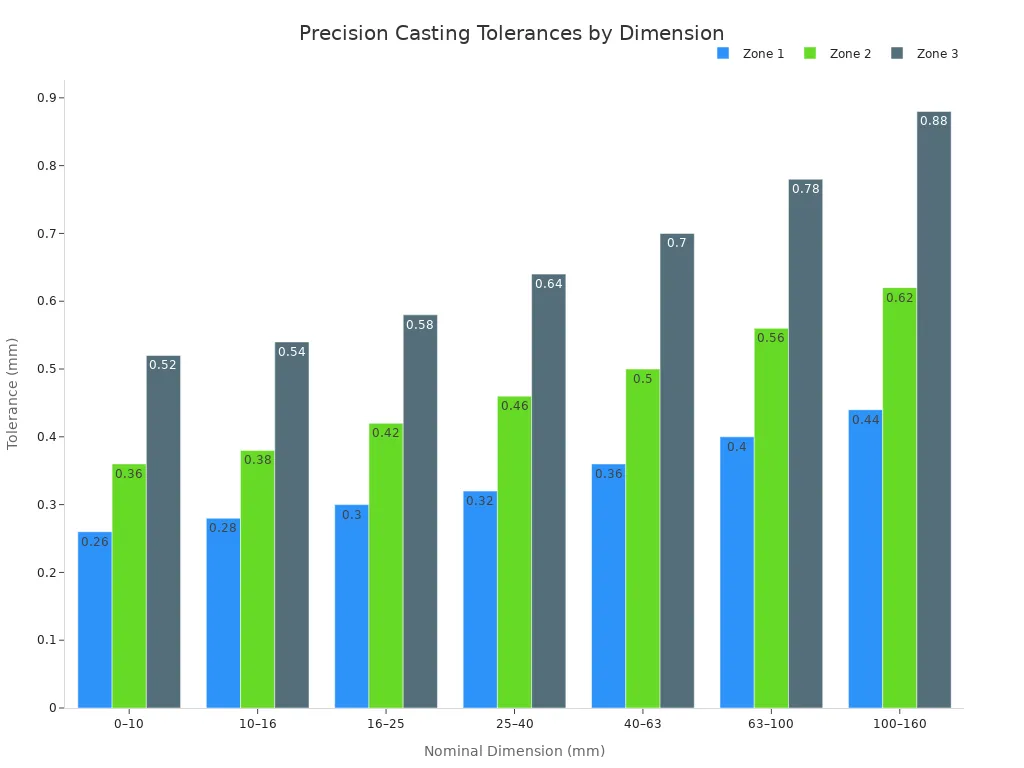
Image Source: https://www.xuxiangtaimetal.com The best cost decision is often a hybrid route. Cast the complex geometry, then machine only the functional surfaces. This approach depends on your drawing, alloy, volume, and inspection criteria.
Evaluating Cost, Lead Time, and Quality
Compare total cost of ownership, not just unit price. Casting usually beats full CNC machining at moderate volumes, and the breakeven point drops for hard-to-machine alloys.
Part Type CNC Machining Cost (USD/pc) Casting Cost (USD/pc, incl. tooling) Breakeven Volume Small aluminum bracket (0.5kg) $18–35 $12–22 (at 1,000 pcs) 400–800 pcs Medium steel housing (5kg) $85–140 $55–95 (at 500 pcs) 300–600 pcs Large ductile iron pump body (25kg) $320–480 $180–260 (at 200 pcs) 120–250 pcs Inconel 718 valve body (3kg) $380–520 $290–410 (at 200 pcs) 80–150 pcs Titanium impeller (1.2kg) $680–950 $420–600 (at 200 pcs) 60–120 pcs Alloys that are expensive to machine, such as Inconel and titanium, have a lower breakeven volume than carbon steel. The per-part machining premium is so high that casting tooling gets amortized faster.
A Canadian mining buyer sourcing 340mm diameter centrifugal casting slurry discharge elbows faced a foundry closure. The part required Ra 1.6µm surface finish on internal wear surfaces — achievable by casting but with expensive tooling modifications and a 14-week lead time. The CNC option (machining from a sand casting blank) reduced lead time to 5 weeks and tooling cost to zero. The per-part cost was 18% higher than the die casting quote, but the eliminated tooling cost and faster delivery meant the project broke even in the first order. Over 18 months of repeat orders, the CNC-from-casting-blank approach saved approximately $240,000 CDN compared to the die casting tooling amortization model.
For complex industrial parts such as pump casings, valve bodies, hydraulic manifolds, and turbine enclosures, the best result almost always combines casting and machining. Casting produces near-net-shape geometry at high volume, reducing material waste and machining time. CNC machining then finishes critical surfaces to exact tolerance. The combined cost is often 30–50% lower than full CNC machining from solid stock.
Certifications and Supplier Vetting
Certifications prove your supplier can hold quality at volume. Require ISO 9001 as the minimum credible certification for any custom casting supplier. Automotive production parts demand IATF 16949, which adds PPAP, APQP, FMEA, SPC, MSA, and control plans. An IATF-certified supplier also satisfies ISO 9001, but the reverse does not qualify for automotive work.
Requirement Details Mandatory certifications for automotive casting suppliers IATF 16949, ISO 9001, and ISO 14001:2015 Quality and delivery expectations 98% to 99% on-time delivery, sub-80 PPM defect rates, and JIT supply chain integration Verification process On-site audits and trial runs verifying IATF 16949 compliance and process capability before high-volume production contracts Verify additional standards separately when they apply. NADCAP covers special processes, ISO 17025 covers in-house testing, ISO 14001 covers environmental requirements, and CMMC covers defense cybersecurity. Always confirm that the supplier’s certificate scope covers the casting work you purchase.
Custom casting gives you a competitive edge in quality, cost, and speed when you specify it correctly. The right Precision Casting Manufacturing Service becomes your engineering partner, not just a vendor. Contact a casting service today to review your drawings and request a quote.
FAQ
What lead time should you expect for custom castings?
You can expect 4 to 8 weeks for tooling and first articles. Production runs typically take 3 to 6 weeks after approval.
What minimum order quantity do casting suppliers require?
Most suppliers accept prototype orders as low as 1 to 20 pieces. Steel tooling becomes economical above 50 pieces for production runs.
How do you verify casting quality before shipment?
You request dimensional inspection reports, material certifications, and non-destructive testing results. Third-party inspection services also verify compliance before shipment.
See Also
Avoid Selecting Incorrect Aluminum Casting Methods Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
-
AuthorPosts

- You must be logged in to reply to this topic.