- This topic is empty.
-
AuthorPosts
-
2026-10-13 at 5:11 pm #12295
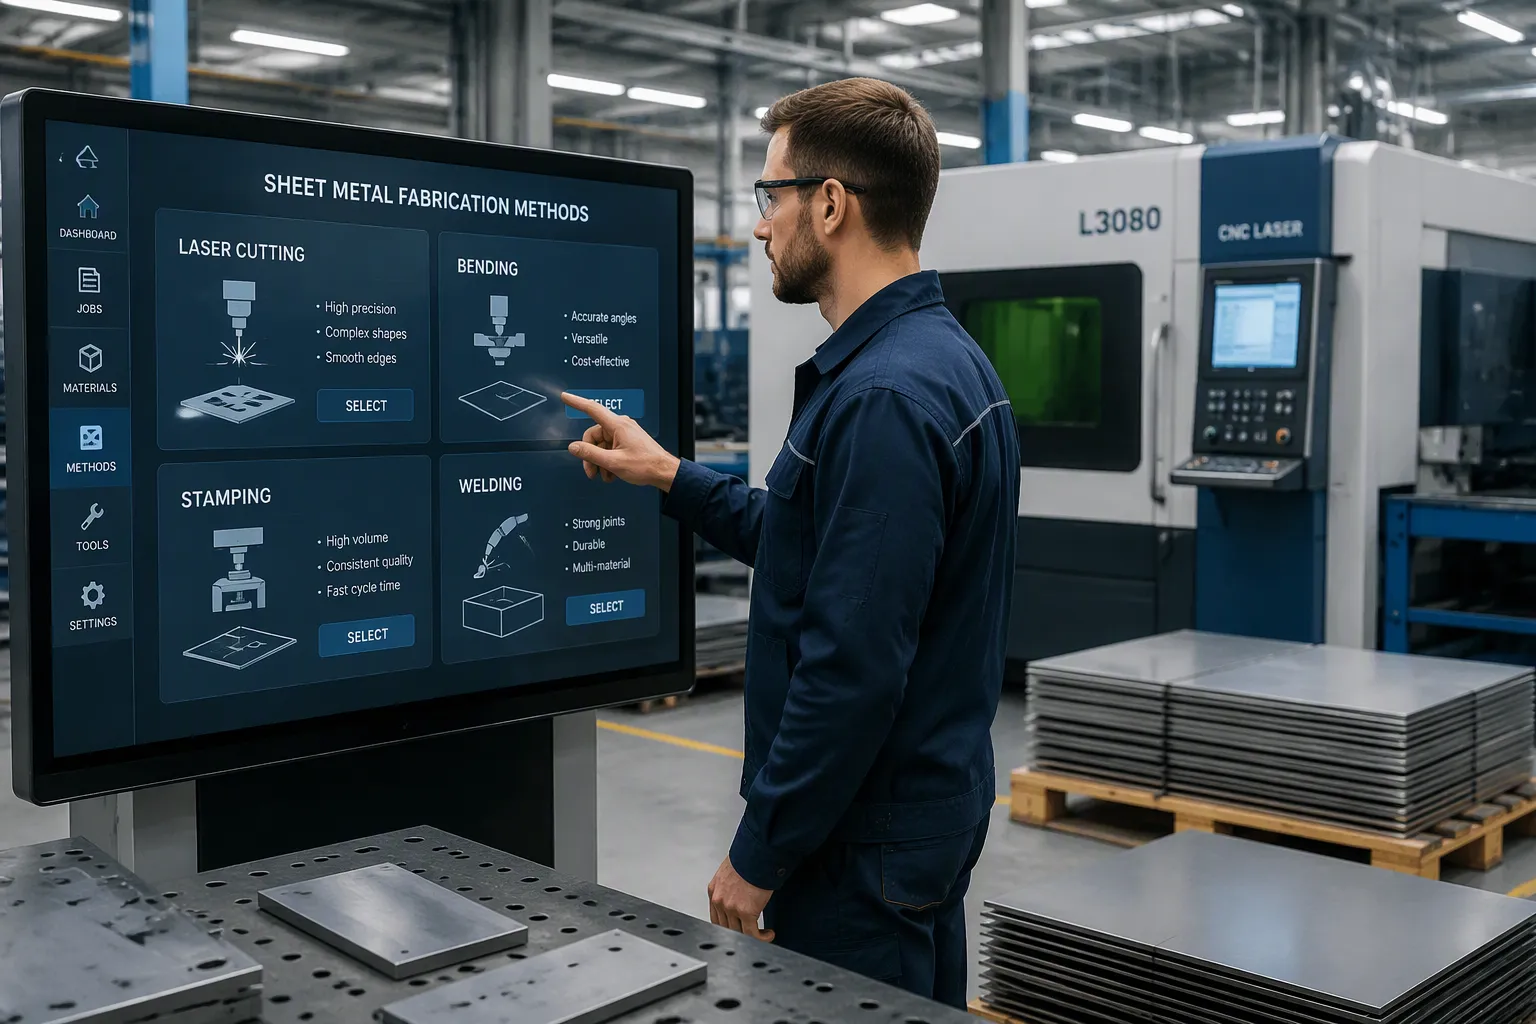
Image Source: https://www.xuxiangtaimetal.com The right fabrication method matches your project’s volume, material, geometry, tolerance, lead time, and budget to a process’s actual capabilities. A mismatch in any single factor can inflate cost, delay delivery, or compromise quality. You should choose the cheapest process that still meets your minimum quality requirements. This guide will help you generate a 1200-word English blog framework for confident process selection.
Key Takeaways
- Match your fabrication method to six key factors: volume, material, geometry, tolerance, lead time, and budget.
- Use a six-step framework to compare processes and find the most cost-effective option.
- Test with a prototype and build a cost model before committing to full production.
Key Factors and Common Processes in Sheet Metal Fabrication
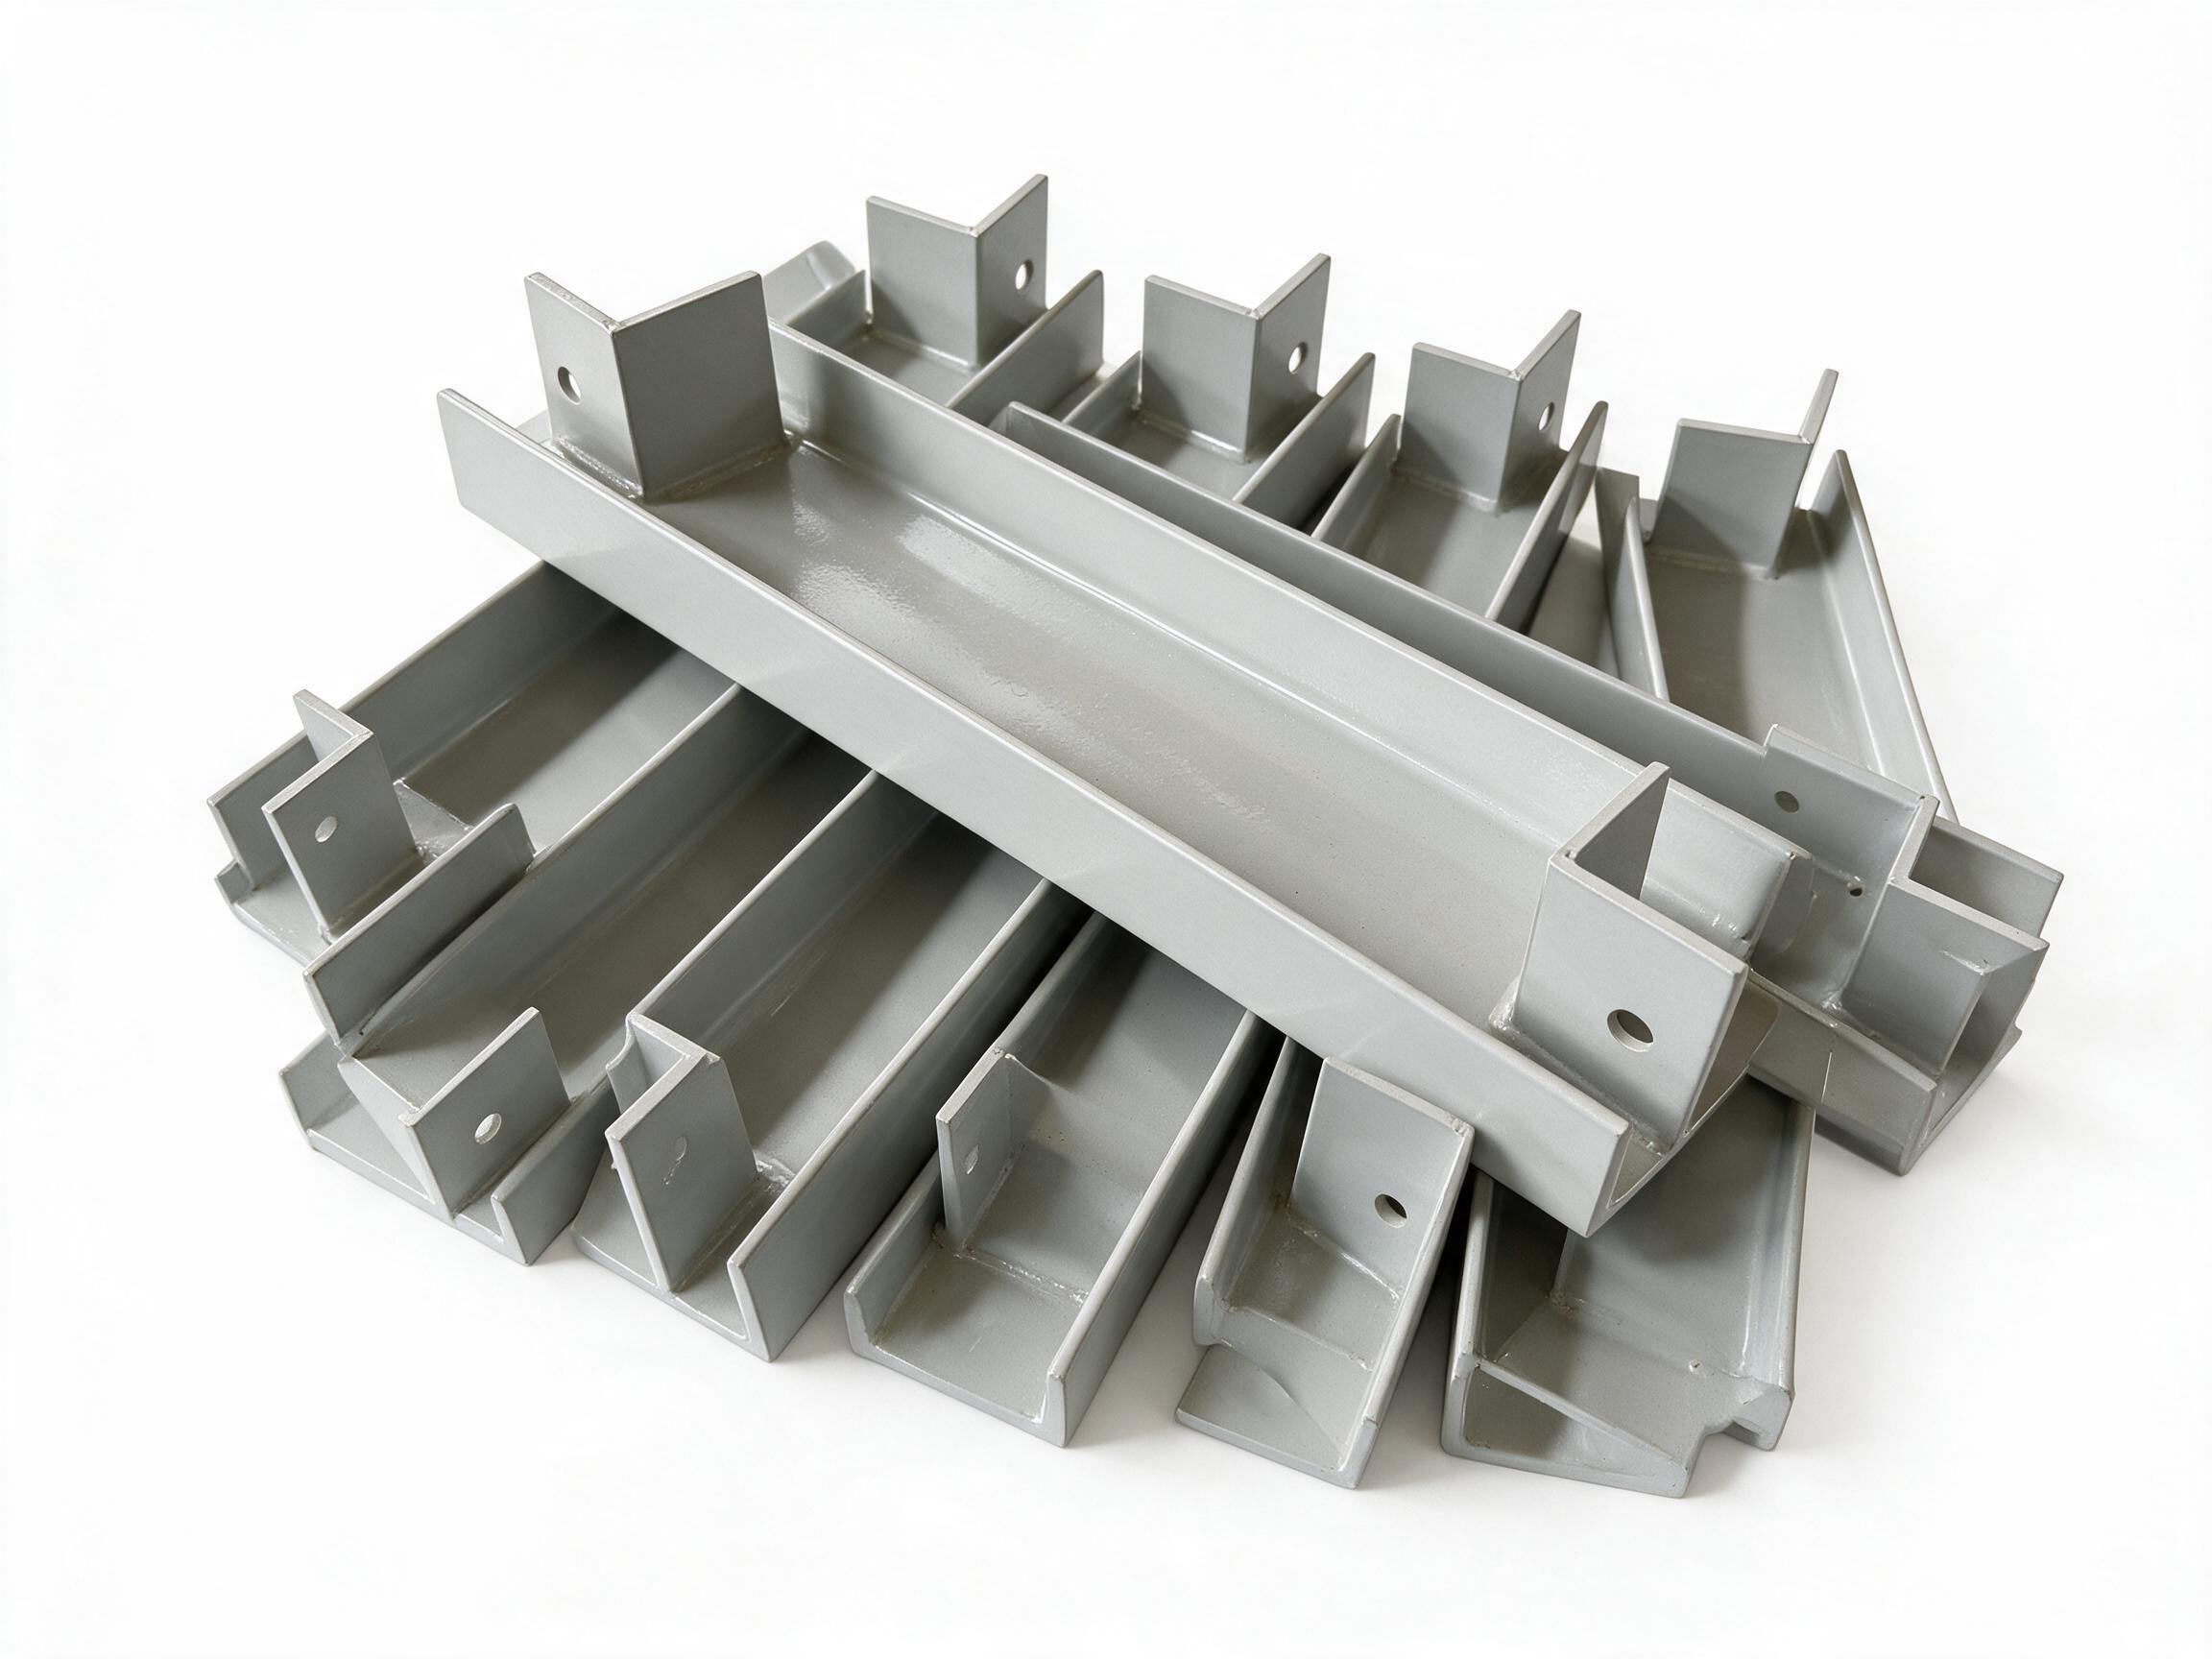
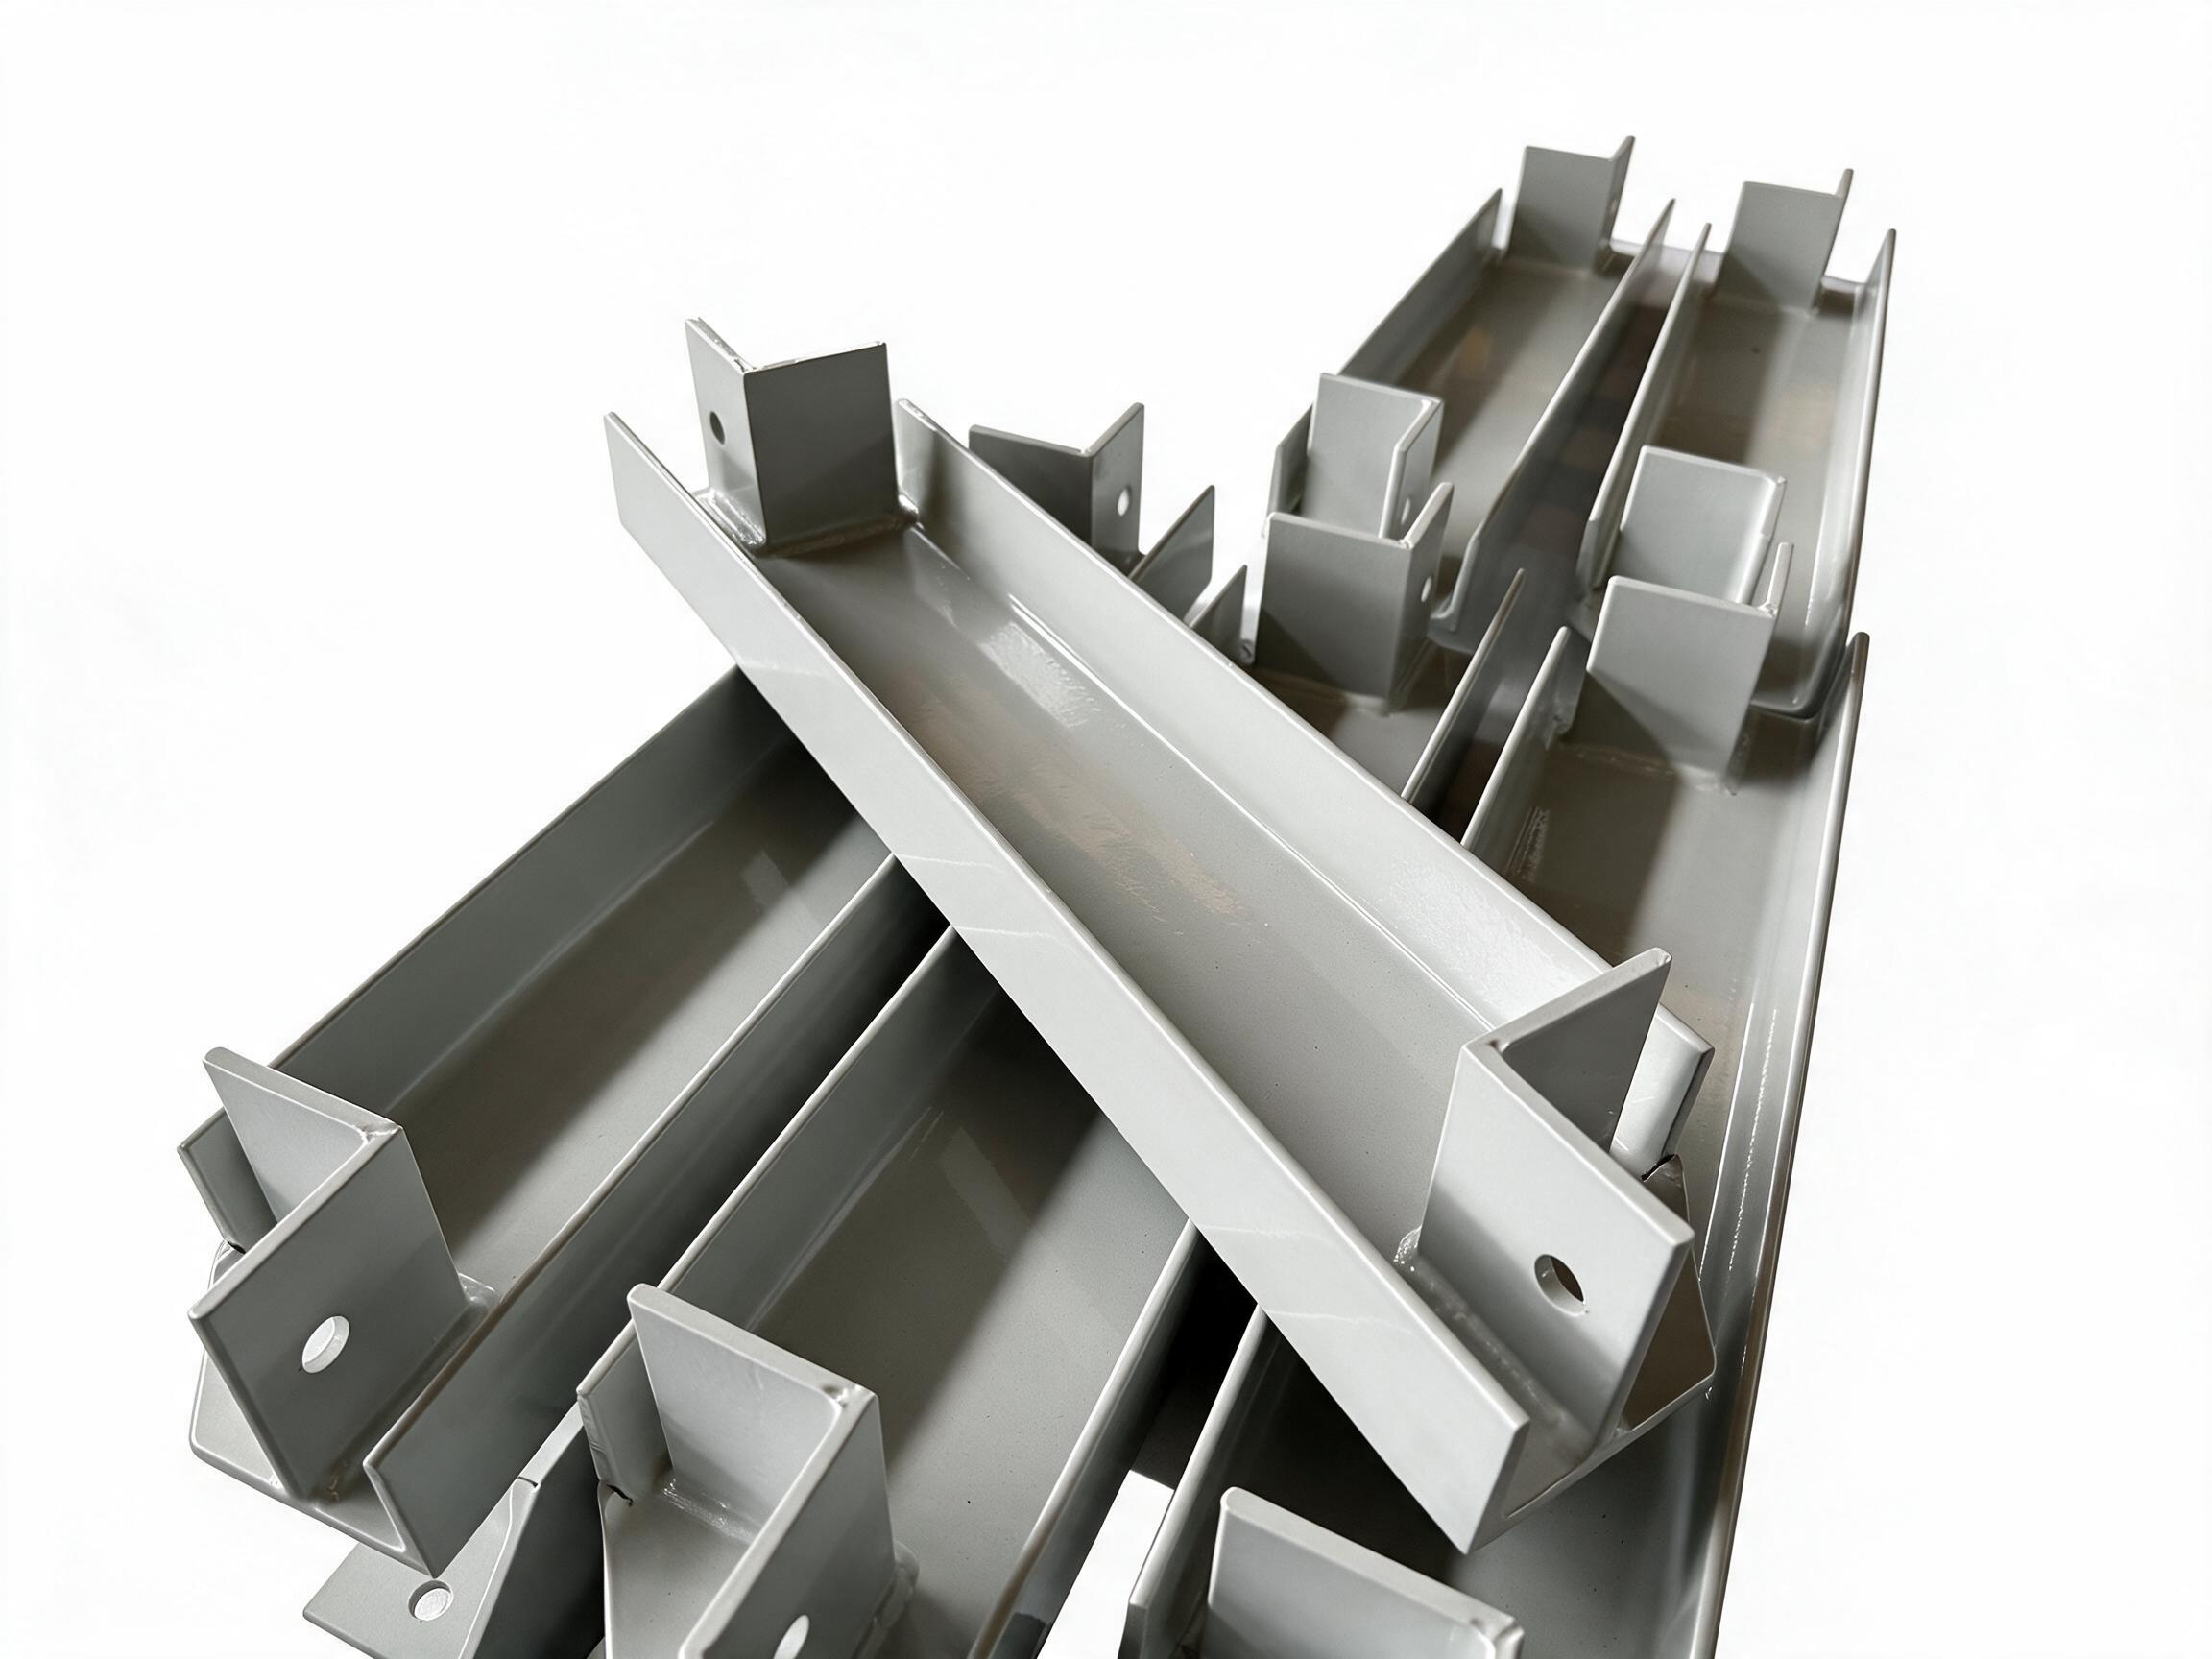
Survey the shop floor before you choose a method. The industry has changed. Modern fiber lasers, collaborative robots, and AI-driven scheduling now define what a fabricator can deliver. Six-kilowatt and twelve-kilowatt lasers handle heavier plate. Vision-guided robots sort blanks with 99.1% accuracy. These technologies expand the envelope of every process.
The decision still comes down to six inputs: volume, material, geometry, tolerance, lead time, and budget. Each input steers you toward or away from a process. Read each factor below, then check the process comparison table at the end.
Production Volume and Run Length
Your first filter is volume. Volume decides how you pay for tooling. Every process has a fixed setup cost and a variable per-piece cost. Laser cutting carries low setup, so you use it for one-offs and small batches. Stamping demands dies, so you reserve it for high-volume production.
Economies of scale apply to sheet metal fabrication costs. Larger production volumes cost less per unit, as processes are replicated and tooling can be reused.
The table below captures the cost behavior across three common approaches:
Process Setup Cost Cost Behavior by Volume Economic Crossover Laser cutting Low setup cost Economical from prototype through medium volumes; unit cost drops sharply as fixed setup is spread across more parts (e.g., a simple zinc-plated steel part falls from ~$29 for one piece to ~$3 at ten pieces, an 86% reduction) Favored at low to medium volumes Stamping / press tooling High upfront investment (commonly $10,000–$60,000 for a progressive die) Reaches the lowest per-piece cost at scale as tooling is reused Typically favored above 10,000–20,000 annual pieces Bending (forming) Setup plus machine time plus labor Each additional bend and tooling change increases total cost; small batches benefit more from simplifying geometry than negotiating unit price Low-volume process Tooling amortization makes the crossover concrete. A $15,000 die spread over 1,500 parts adds $10.00 per part. The same die over 150,000 parts adds only $0.10 per part. You pass the stamping break-even somewhere between 10,000 and 20,000 pieces per year. Laser cutting and CNC bending cost less below that range because they avoid custom tooling.
Material Type and Thickness
Material type narrows the process list quickly. Thin sheet metal from 24 to 28 gauge cuts and bends with ease. Use it for appliance panels and electronics enclosures. Medium stock from 18 to 22 gauge balances strength and formability for automotive and HVAC parts. Thick stock from 10 to 16 gauge supports structural frames and machinery. Thicker plate may force you toward plasma or waterjet.
Formability follows the alloy. Aluminum and copper stretch without cracking. Stainless steel needs more force and stiffer equipment. Corrosion resistance matters too. Stainless and aluminum survive outdoor exposure; mild steel needs powder coating or plating. Material prices swing with metal markets, so successful fabricators lock in reliable suppliers and use transparent pricing. Match the material’s properties to the machine’s capacity.
Fiber laser cutting sets the boundary for many jobs. High-power fiber systems in 2026 process these maximum thicknesses efficiently:
Material Maximum efficient thickness Carbon steel ~1 in Stainless steel slightly over 1 in (~1.1 in) Aluminum ~1.0–1.2 in Brass ~5/8 in Copper ~1/2 in 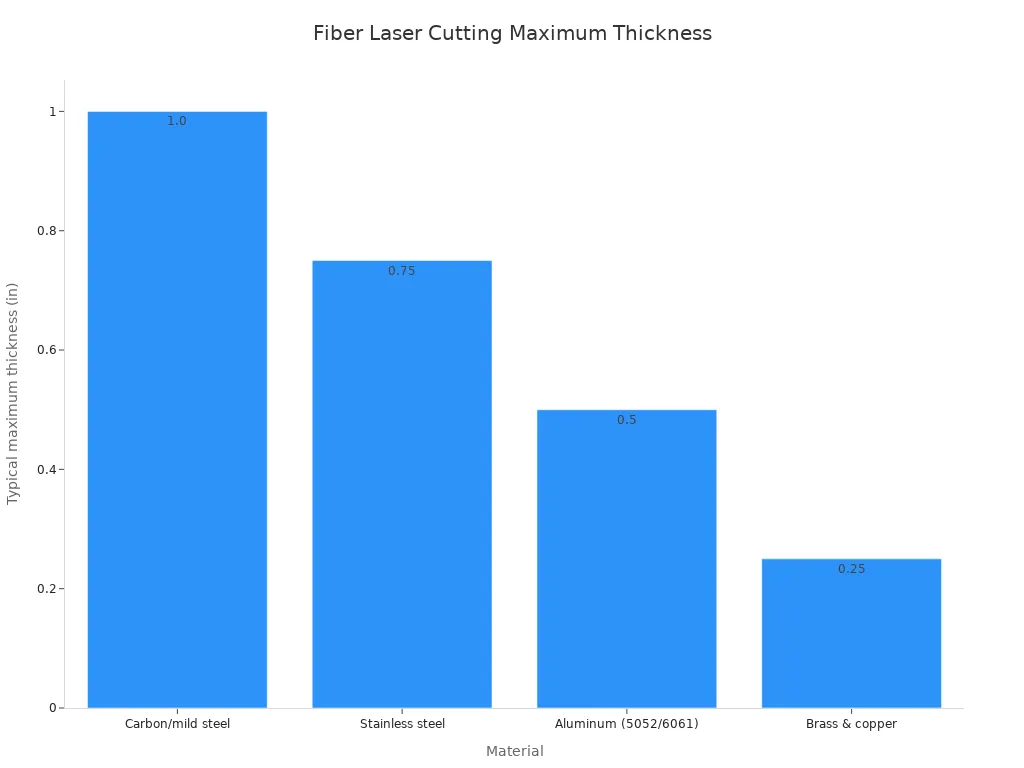
Image Source: https://www.xuxiangtaimetal.com Plasma or waterjet take over above those limits. Laser offers the best blend of edge quality and speed below them. These numbers shift with machine power and assist gas, so verify with your fabricator.
Geometry, Bend Radii, and Design Complexity
Geometry dictates forming difficulty. A flat pattern with simple bends works on a CNC press brake. Deep cavities, ribs, or flanges require stamping dies. Complex multi-plane features may need progressive tooling.
The rule for 5052 aluminum is simple: multiply thickness by 0.8. The table shows recommended minimum inside radii for three common gauges:
Material Thickness Minimum Inside Bend Radius Aluminum 5052 1 mm 0.8 mm Aluminum 5052 2 mm 1.6 mm Aluminum 5052 3 mm 2.4 mm These values are minimums, not design targets. Larger radii reduce cracking risk. Bending across the grain and choosing a softer temper also help.
Match the enclosure design to the fabrication process: use flexible cutting and bending for prototypes and low volumes, and reserve tooling-heavy stamping for designs whose lifetime volume justifies the die investment. Simplify geometry and standardize features so the design works with the process rather than fighting it.
Tolerances and Surface Finish
Tolerances protect fit and function. Laser cutting holds tight dimensions with clean edges. Waterjet produces smooth, burr-free edges, but slower. Plasma leaves striations and dross that demand grinding. Shearing creates raw edges that need deburring.
Precision edges demand tight tolerance. Laser cutting delivers Ra 3.2–6.3 µm without secondary work. Plasma often cannot. Tight tolerances raise cost. Specify them only where needed.
Lead Time and Cost Targets
Lead time now acts as a gatekeeper. Customers once accepted 12–16 week schedules. Buyers expect 6–8 weeks or less in 2026. Smart factories using AI scheduling see 12% more throughput. Remote monitoring improves CNC uptime by 18%. These gains compress the time from drawing to delivery.
Prototype turnaround with laser cutting and CNC bending now looks like this:
Aspect Lead Time / Detail Typical prototype production A few days rather than weeks Single parts 2–7 days Multi-bend setups Add hours Key dependencies Part complexity and material availability Cost targets extend beyond unit price. Buyers evaluate delivery reliability, quality consistency, and engineering support. Certifications like ITAR or UL create access barriers. A low quote from an outdated shop can become a costly delay later.
Cutting Methods: Laser, Plasma, Waterjet, Shearing
Cutting converts flat sheets into blanks or finished profiles. Laser leads in speed and precision. Plasma offers lower cost but rougher edges. Waterjet cuts almost anything without heat. Shearing remains the fast choice for straight-line production.
The differences at 6 mm mild steel are clear:
Process Cutting Speed (6 mm Mild Steel) Edge Quality Fiber Laser 3–5 m/min (fastest) Excellent, smooth and square, essentially burr-free; Ra 3.2–6.3 µm; rarely needs finishing Plasma 2–3 m/min (fast) Rough; striations, rounded top bevel, bottom dross requiring grinding; almost always needs secondary finishing Waterjet 0.3–0.8 m/min (slowest) Very good; smooth and burr-free, no heat-affected zone; slow cutting gives laser-like finish, fast cutting leaves slight frosted texture Additional speed comparisons confirm the ranking:
- Thin material under 6 mm magnifies the speed gap. Laser runs 5–10 times faster than waterjet and about 1.5–2 times faster than plasma.
- Waterjet sits at the bottom for speed, which raises its cost per part.
- Laser cuts with a narrow heat-affected zone of only 0.1–0.5 mm.
- Plasma leaves the roughest edge and needs grinding or deburring.
- Waterjet leaves a smooth edge but no heat-affected zone, preserving material properties.
Shearing still has a place. It beats laser on both speed and cost for high-volume production of straight-line cuts. This table shows when each one fits:
Factor Shearing Laser Cutting Cost Lower Higher Speed for straight-line cuts Very fast, especially in high-volume production Generally slower for basic straight cuts Best use case High-volume production of standardized parts and simple cuts Intricate designs, diverse materials, rapid prototyping, high precision Cut type limitation Limited to straight-line cuts Can handle complex and intricate cuts Shearing prioritizes speed and low cost for high-volume simple cuts, while laser cutting focuses on intricate designs and high precision across diverse materials.
Forming Methods: Bending, Stamping, Roll Forming
Forming gives sheet metal a third dimension. Bending uses a press brake and standard V-dies. It costs little to start and suits prototypes and short runs. Stamping relies on shaped dies and becomes economical only at scale. Roll forming feeds coils through rollers for long, constant cross-sections.
Design complexity shifts the balance between stamping and flexible bending. This table shows the boundary:
Design complexity Stamping/forming approach CNC/flexible bending suitability Low–medium (simple 2D shapes, holes, simple bends) Blanking/piercing or basic bending/forming Suitable for low-volume/prototype enclosures Medium (angles, flanges, ribs; consistent wall thickness) Bending/forming within stamping, with DFM simplification of bends Can produce these without dedicated die tooling in flexible CNC bending High (deep hollow shapes, intricate multi-feature parts) Deep drawing, four-slide, or transfer/progressive die stamping CNC bending alone is insufficient; dedicated stamping tooling is needed Bending costs rise with every bend and tooling change. Stamping amortizes its die over each part. Roll forming generates high output and low per-part cost for profiles like channels and rails. Modern electric press brakes also cut energy use by half compared with hydraulic models, so your choice can lower operating costs.
Joining Methods: Welding, Riveting, Clinching, Adhesive Bonding
Joining methods lock components together. Welding produces strong permanent bonds. TIG works well on thin stainless. MIG handles thicker steel. Laser welding minimizes distortion. Riveting joins parts that cannot tolerate heat. Clinching presses overlapping metal into a mechanical lock. Adhesive bonding spreads loads and seals surfaces, but needs clean surfaces and curing time.
Choose based on material, load, and service environment. Enclosures use spot welding and clinching. Structural frames rely on MIG or TIG steel welding.
Process Comparison Table
Use this reference when you stack processes side by side. It covers the typical application and the economic sweet spot for each method:
Process Typical application/indication Economic note Stamping Most common sheet-metal process; used in nearly all sheet-metal hardware parts, often with other operations. High upfront tooling; favors large runs Punching Makes holes or perforations so parts can be fastened to other components. Fast; good for smaller to medium parts Bending Produces U- or V-shaped angles and curves; used for many commercial products and hardware. Low tooling; ideal for prototypes/low volume Deep drawing Creates cup-like or pan-like deep cavities, typically by cold stretching. Requires dies; for higher volumes Rolling Uses rollers/progressive tooling to shape sheet metal; effective for high-volume manufacturing from coils. Efficient for long, curved profiles Welding Joins metal sections with heat and pressure; common variants are TIG, MIG, and stick welding. Manual or automated; labor heavy Shearing Cuts or tears sheet metal; edges usually require deburring or tumbling. Low cost, fast straight cuts Laser cutting High-precision cutting suited to small or intricate parts with minimal damage. Low setup; prototypes to medium volume Plasma cutting High-heat cutting at lower cost than laser; leaves slag that must be removed. Good for thicker plate Waterjet cutting Uses ultra-high-pressure water; can cut many materials and thick sheets for large-scale commercial parts. Slow but versatile and no HAZ How to Pick the Right Method: Generate a 1200-Word English Blog Step-by-Step Selection Framework
Image Source:https://www.xuxiangtaimetal.com You now have the process landscape in front of you. The next task is to match those capabilities to your specific project. The six-step framework below forces a structured comparison. Working through each step in order prevents the costly habit of jumping to a favorite process before checking the data.
Start by writing down your constraints. Filter processes one at a time. Each step narrows the field. You will eliminate laser cutting from a 100,000-part job just as quickly as you will eliminate stamping from a 12-piece prototype. That clarity is the value of the framework.
Decide your documentation method at the outset. A written record helps you justify the choice later. Generate a 1200-word English blog that captures the decision rationale for each process you consider. That document becomes a reference for the next project and a communication tool for stakeholders.
Step 1: Define Volume and Timeline
Volume drives the first filter. You should set a realistic quantity range for the program. That range determines whether tooling-based processes can pay for themselves. Lead time runs a close second. Split your timeline into time-to-first-part and production throughput. Tooling-based processes take weeks to deliver first parts. Toolless processes can produce within days.
Follow this sequence to establish your parameters:
- Define the part requirements: geometry, material, volume, tolerance, and cost targets before evaluating any process.
- Filter by production volume: use volume as the primary filter, since it determines whether tooling-based or toolless processes are viable.
- Evaluate lead time: treat lead time as a primary filter; split it into time-to-first-part and production throughput.
- Compare cost structure: weigh fixed tooling capitalization against variable per-unit costs. Custom stamping, blanking, and bending dies run from $500 to $20,000 or more. Tool-less laser cutting and CNC press brakes avoid that capital.
- Check material, tolerance, and finish constraints: confirm the process can meet ductility, edge quality, and coating requirements.
Compare your volume against the break-even table. The crossover from flexible fabrication to stamping depends on part complexity:
Part Complexity Typical Break-Even Volume (parts) Simple flat parts (few holes, no forming) 2,000–5,000 Moderate complexity (multiple bends + punched holes) 3,000–8,000 High complexity (deep draws, forming features) 500–2,000 Worked example (general) ~2,857 A simple bracket with four holes and two bends could justify stamping at 4,000 pieces. A deep-drawn enclosure might justify tooling at 800 pieces. The high-complexity scenario shifts the break-even down because laser cutting requires a separate setup for every bend and hole, while a stamping die performs all operations in one press stroke.
Your timeline can override the volume math. A five-day deadline for 500 parts eliminates stamping. Laser cutting and press brakes will deliver. A 50,000-piece annual volume with a 12-week tooling lead time favors stamping. Calculate both volume and timeline together before you move forward. You can generate a 1200-word English blog that starts with these two numbers, because they constrain every process option that follows.
Step 2: Identify Geometry Constraints
Geometry determines whether a part belongs on a press brake or in a die. You should review your model for features that create risk. Sharp inside corners cause stress concentrations. Wrong hole sizes break tooling. Missing bend allowance produces dimensional errors. These defects surface during production and drive rework costs.
The following mistakes account for most fabrication errors:
Mistake Category Financial / Operational Impact Wrong material selection Accounts for 51% of fabrication errors, leading to part failure, rework, and wasted material costs Poor cutting techniques Causes about 50% of weld problems in sheet metal, resulting in ill-fitting parts, scrap, and rework Bad welding quality Responsible for roughly 30% of structural failures; good welding can make structures up to 35% stronger Neglected equipment calibration Up to 20% increase in product rejection rates, 15% higher safety incident risk, and up to 30% higher maintenance costs Poor communication / training gaps Skilled teams can cut mistakes by up to 30%; good communication can make projects 25% faster; new tools can cut maintenance costs by 15–25% Apply these design rules during the geometry review:
- Use fillets and radii on inside corners to prevent stress concentrations and cracking during bending.
- Keep hole diameter at or above 1.5× material thickness to avoid punching defects and tool breakage.
- Calculate bend allowance and deduction for your specific material, thickness, and tooling.
- Maintain minimum flange width of 3× material thickness for stable bending.
- Place holes at least 2× material thickness away from bends and edges to prevent cracks and deformation.
Geometry also tells you which forming process suits the part. Low-complexity shapes with simple bends work on CNC press brakes. Deep cavities, ribs, and flanges require progressive dies. A deep-draw feature shrinks your process list to stamping or hydroforming. A part with only two parallel bends works well on a laser cutter and press brake.
Step 3: Confirm Material and Thickness
Material choice follows geometry in the sequence. Ductile metals dominate sheet metal fabrication. Low-carbon steel, stainless steel, aluminum alloys like 5052-H32, brass, and copper all form well. Materials that lack ductility do not belong in this process group.
Material selection errors cause more fabrication defects than any other single factor. The 51% figure from the error analysis means you cannot treat material as an afterthought. Confirm the grade with your supplier. Check the temper. Verify the sheet thickness against the machine capacity. A 3 mm aluminum part requires a different laser power setting than a 0.8 mm steel part.
Thickness affects every downstream decision. Thin gauges from 24 to 28 bend easily but flex under load. Thick stock from 10 to 16 gauge supports structural frames but requires more force and heavier equipment. Match the thickness to the process envelope. Fiber lasers handle carbon steel up to 1 inch efficiently. Plasma and waterjet take over above that range.
Formability follows the alloy chemistry. Aluminum 5052 stretches well and accepts tight radii. Stainless steel needs more press force and stiffer tooling. Copper and brass cut cleanly but cost more per pound. Include corrosion resistance in the selection. Mild steel requires powder coating or plating for outdoor use. Stainless and aluminum survive exposure with minimal treatment.
Document the material decision in your process write-up. State the material grade, the sheet thickness, and your justification. This record prevents a future engineer from substituting a cheaper alloy and causing rework. You can also generate a 1200-word English blog that preserves the full material rationale for future projects.
Step 4: Specify Tolerances and Finish
Tolerance requirements distinguish between processes. Sheet metal fabrication holds feature tolerances of ±0.1 to ±0.25 mm, but that capability depends on the process and the feature. Laser cutting delivers clean edges with Ra 3.2–6.3 µm finish. Plasma leaves striations and dross. Waterjet produces smooth edges but runs slower.
Do not over-specify tolerances. Every added decimal place of precision raises the quoted cost. Call out tight tolerances only on functional surfaces. Let the rest of the part sit at standard values.
Surface finish requires the same precision in specification. Anodizing outperforms powder coating on aluminum parts that need wear resistance. Powder coating wins when you need color flexibility. The table compares the two systems:
Surface Finish Attribute Powder Coating Anodizing Typical coating thickness 60–120 µm 5–25 µm (hard anodize up to 50 µm) Surface hardness Moderate (pencil hardness H–2H) High (hard anodize can exceed 400 HV) Color / appearance range Virtually unlimited RAL/Pantone, gloss, texture Limited (clear, black, bronze, limited dyes) Dimensional impact on parts Noticeable build-up; affects fits Minimal thickness change; suitable for tight tolerances Wear / abrasion resistance Good impact, moderate abrasion Superior abrasion resistance Corrosion resistance Good to excellent with pretreatment Excellent on aluminum, especially when sealed Apply the selection logic directly:
- Choose Type II anodizing when the part is aluminum, corrosion protection is needed, and a clear or decorative appearance is desired.
- Choose Type III hardcoat anodizing when wear resistance matters and the design can accommodate dimensional effects.
- Choose powder coating when you need a broad color range, a specified gloss or texture, and coating buildup is acceptable.
Remember the color-matching caveat. Anodized color varies with alloy, surface condition, oxide layer, dye, sealing, and lot. An anodized part will not exactly match a powder-coated part, even with a similar color request. Record the finish specification next to the tolerance callouts. The coating thickness changes part dimensions. A 100 µm powder coat on a mating surface requires clearance in the design. You should generate a 1200-word English blog that records the coating thickness and its dimensional effect on mating parts.
Step 5: Run a Cost Model and Compare
You have defined volume, geometry, material, tolerance, and finish. Now you can price the candidates. A cost model must include more than the quoted unit price. Build a complete cost picture with these factors:
Cost factor Cost-model implication Raw materials Include grade, procurement price, processing difficulty, and corrosion resistance Design complexity Count bends, welds, stamped features, tolerances, and DFM effects Process/equipment Compare laser cutting precision with stamping tooling at the target volume Finishing Add powder coating, anodizing, galvanizing, plating, and handling labor Volume/scale Amortize setup and programming costs over quantity Labor/automation Price skilled labor and offset with CNC/automation investment Scrap/efficiency Include nesting waste, material utilization, and disposal cost Procurement/supply chain Factor in material price changes and delivery coordination Contrast the two leading candidates in a matrix. The table shows how the same cost factors behave differently:
Cost factor Laser cutting Stamping Tooling Low or no dedicated tooling; suits prototypes and design changes Dedicated dies; cost justified by repeat volume and frozen design Production volume Best for low volumes, bridge production, or frequent geometry changes Best for stable, repeat production; unit cost falls as tooling amortizes Material utilization Nesting efficiency and cut path determine scrap Strip layout, carrier design, and part orientation determine scrap Secondary operations May require deburring or other finishing Tapping, welding, plating, or painting can change total cost Tolerance/inspection Tight tolerances on nonfunctional features add avoidable cost Die design, tool maintenance, and in-process checks drive tolerance cost Total cost basis Use unit price plus scrap, inspection, packaging, and revision risk Compare on the same total-cost basis, not isolated press operation price Use the same total-cost basis for every process you compare. A laser quote includes programming, machine time, assist gas, and deburring. A stamping quote includes die design, strip layout, press time, and tool maintenance. Missing any line item distorts the comparison.
The break-even formula summarizes the crossover logic:
Break-Even Quantity = (Stamping Tooling Cost – Laser Setup Cost) / (Laser Unit Cost – Stamping Unit Cost)
Stamping tooling cost includes the non-recurring engineering to design, fabricate, and qualify the die set. Laser setup cost includes CAD/CAM programming, nesting, and machine setup. Laser unit cost covers machine time, assist gas, labor, and raw sheet material. Stamping unit cost covers coil stock, press operating time, and die maintenance. No universal crossover quantity exists. Obtain project-specific quotations before you decide.
Run the model for two or three process options. You can then generate a 1200-word English blog that documents the cost comparison in plain language. The written analysis helps stakeholders understand why tooling wins at scale.
Step 6: Plan the Prototype-to-Production Transition
The final step connects the process choice to the production ramp. Laser cutting and CNC bending serve prototypes and low-volume runs without tooling risk. When you freeze the design and approve full production, you can transition to stamping if volume justifies it. Plan the transition before the prototype order ships.
Bridge production is a legitimate strategy. Use laser cutting for the first 1,000 parts while the die is in fabrication. Ship those parts to satisfy early orders. When the tooling arrives, switch to stamping for the remaining 49,000 parts. This approach avoids production gaps and spreads tooling cost across the full schedule.
Design freeze matters more than schedule pressure. Every revision after the die order invalidates the tooling investment. Complete the design review, approve the drawing, lock the geometry, and only then commit to hard tooling. Prototypes exist to reveal design flaws. Take the time to make corrections while the laser still cuts parts cheaply.
Validate the finish specification during the prototype run. Powder coating and anodizing produce different appearances on the same geometry. Confirm the coating color and texture on real parts. That step prevents a rejection during full production. The same validation applies to tolerances. Measure prototype parts against the engineering drawing. Adjust process parameters before you scale.
The framework ends where production begins. Follow this sequence, and you can generate a 1200-word English blog that captures the entire decision trail. Use that document with the comparison table from the previous section. Together they form a repeatable process selection tool.
The right method matches your volume, material, geometry, tolerance, lead time, and budget. Apply the six-step framework and comparison table as a repeatable decision tool. These tools prevent mismatches that inflate cost or compromise quality. Run a prototype and build a cost model before committing to full production.
Submit your 2D/3D drawings for DFM review, process assessment, and quotation. Your fabrication partner will confirm the process choice against real machine capability.
FAQ
Q: What volume justifies stamping over laser cutting? A: Part complexity determines the crossover. Simple flat parts require 2,000–5,000 units. Deep-drawn parts justify tooling at 500–2,000 units.
Q: What tolerance can laser cutting hold? A: Features hold ±0.1 to ±0.25 mm. Edge finish reaches Ra 3.2–6.3 µm without secondary operations.
Q: Can I prototype with one process and produce with another? A: Yes. Laser cutting validates prototypes. Stamping produces final parts when volume justifies the die investment.
FAQ
What volume justifies stamping over laser cutting?
Part complexity sets the crossover. Simple flat parts need 2,000–5,000 units. Deep-drawn parts justify tooling at 500–2,000 units.
What tolerance can laser cutting hold?
Laser cutting holds ±0.1 to ±0.25 mm on features. Edge finish reaches Ra 3.2–6.3 µm without secondary operations.
Can I prototype with one process and produce with another?
Yes. Laser cutting validates prototypes. Stamping produces final parts when volume justifies the die investment.
Submit your 2D/3D drawings for DFM review, process assessment, and quotation. Your fabrication partner will confirm the process choice against real machine capability.
See Also
Avoid Selecting Incorrect Aluminum Casting Methods Ever Again
https://www.xuxiangtaimetal.com
Qingdao Xuxiangtai Machinery -
AuthorPosts

- You must be logged in to reply to this topic.